
 +91 9606018355
 sales@safeautomations.com
VIBRATING CONVEYOR
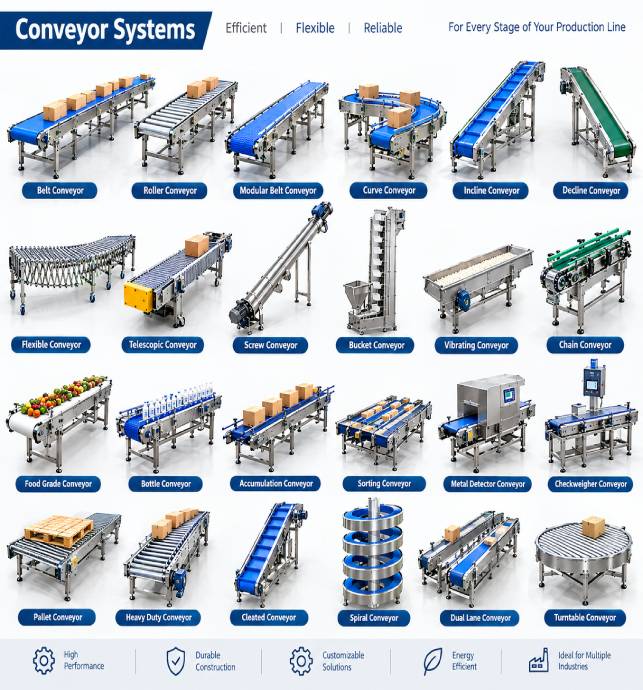
VIBRATING CONVEYOR
Automated Material Handling & Conveyor Systems
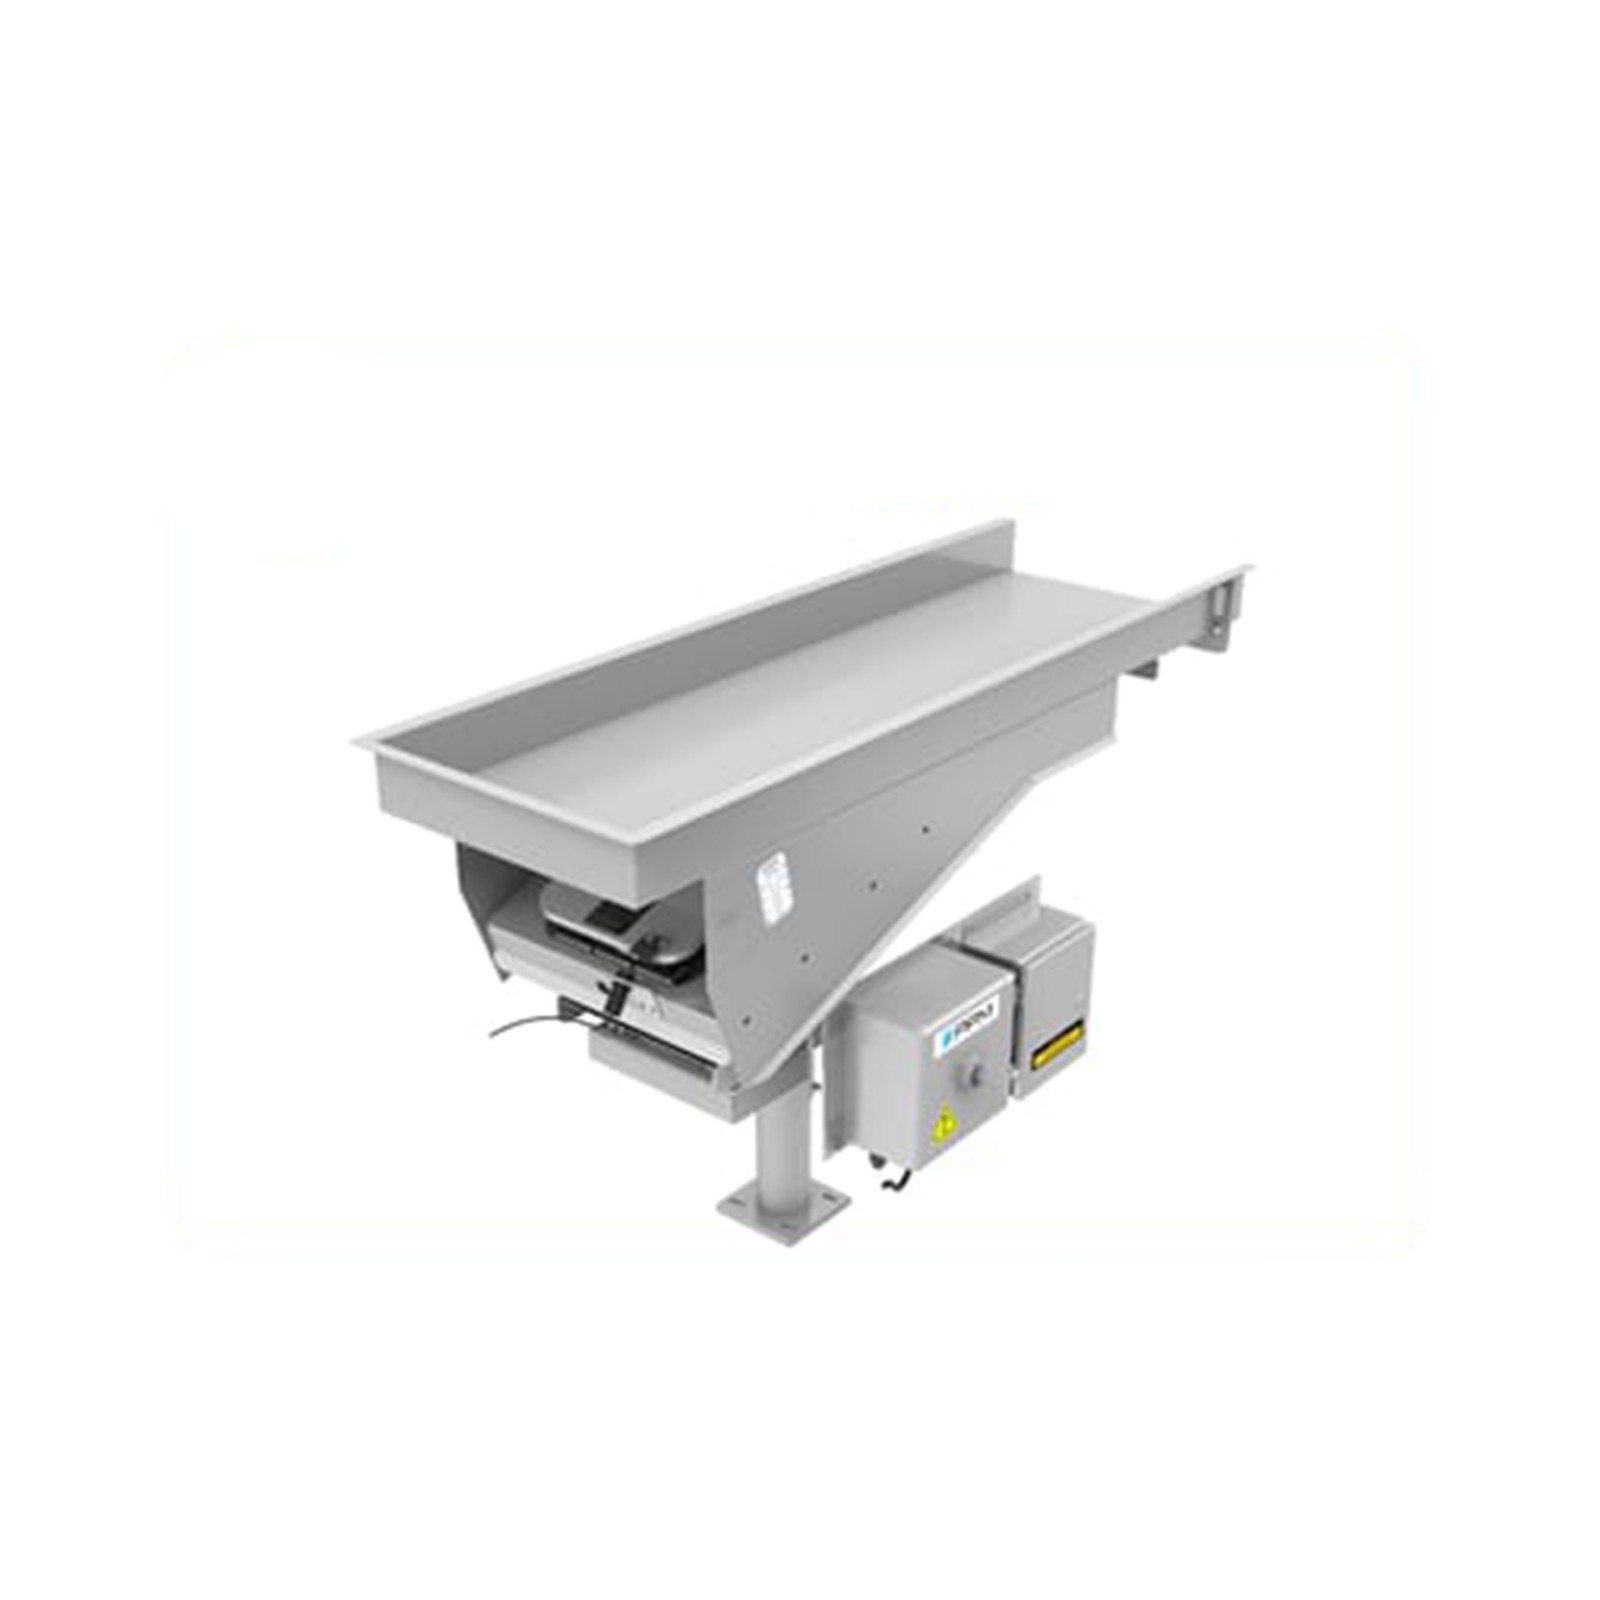
Vibrating Conveyors are designed to efficiently transport bulk materials and products using controlled mechanical or electrical vibrations. The vibrating trough or tube creates smooth directional and upward movement, ensuring consistent material flow.
Their reliable conveying action makes them suitable for handling loose materials, powders, granules, and various products across food processing, manufacturing, and industrial applications.