+91 9606018355
+966 13 363 0010
sales@safeautomations.com
Home
About
Products
Product Inspection System
Automation & Robotics
Conveyor Systems
Packaging System
Coding & Marking System
Food Processing Machines
Services
Turnkey Solutions
Project Engineering / EPCM
Customer Service
Resources
Gallery
Events
News & Updates
Contact
Get A Quote
Conveyor Systems
home
Products
Conveyor Systems
Discover Our Products
Product Quality Inspection
Automation & Robotics
Conveyor Systems
Packaging System
Coding & Marking System
Food Processing machines
Expert Help For You
+91 9606018355
sales@safeautomations.com
Conveyors
Conveyors
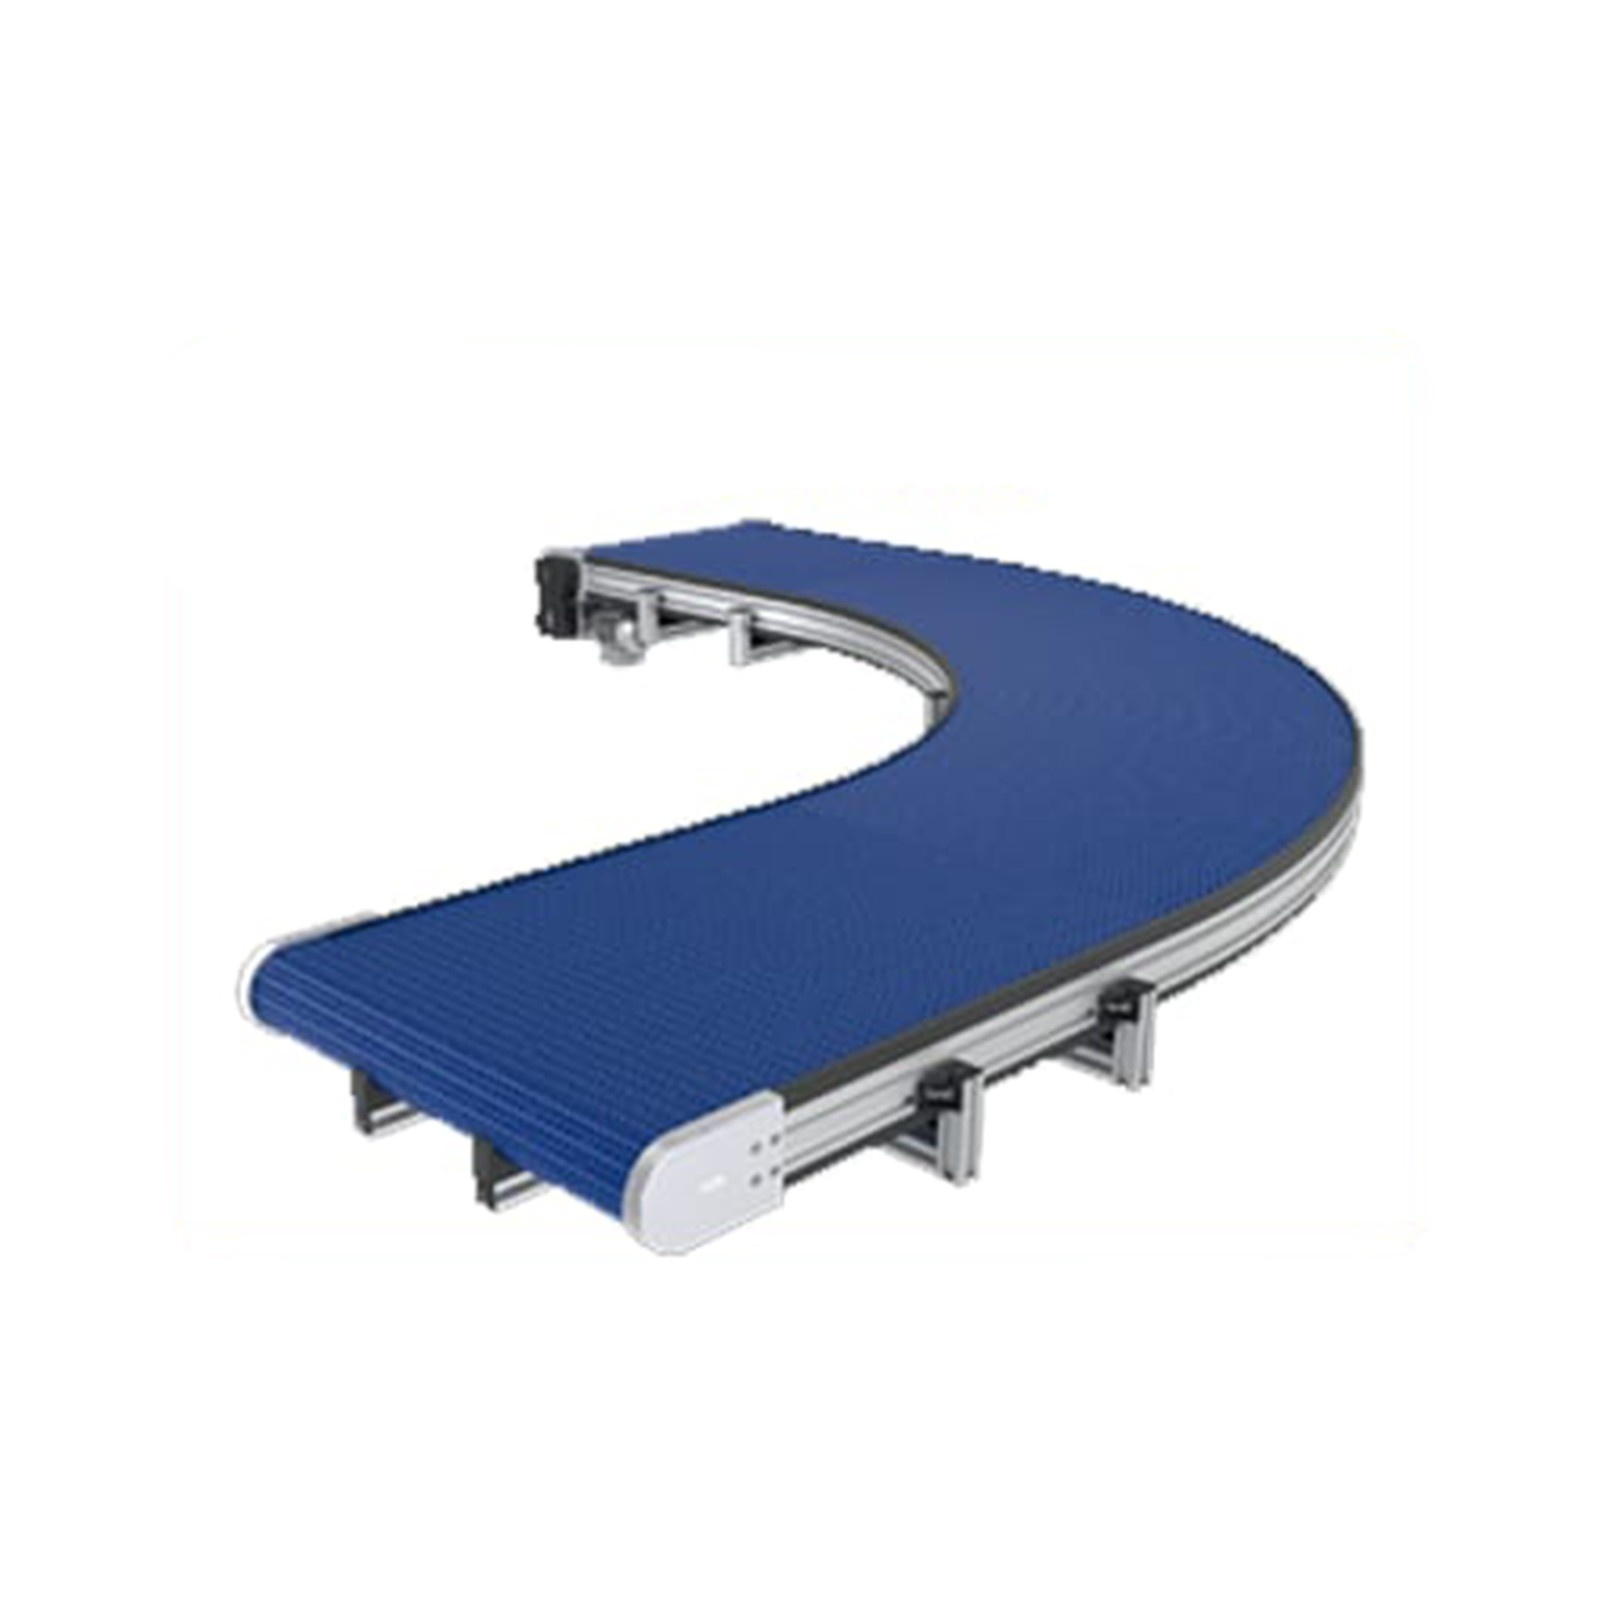
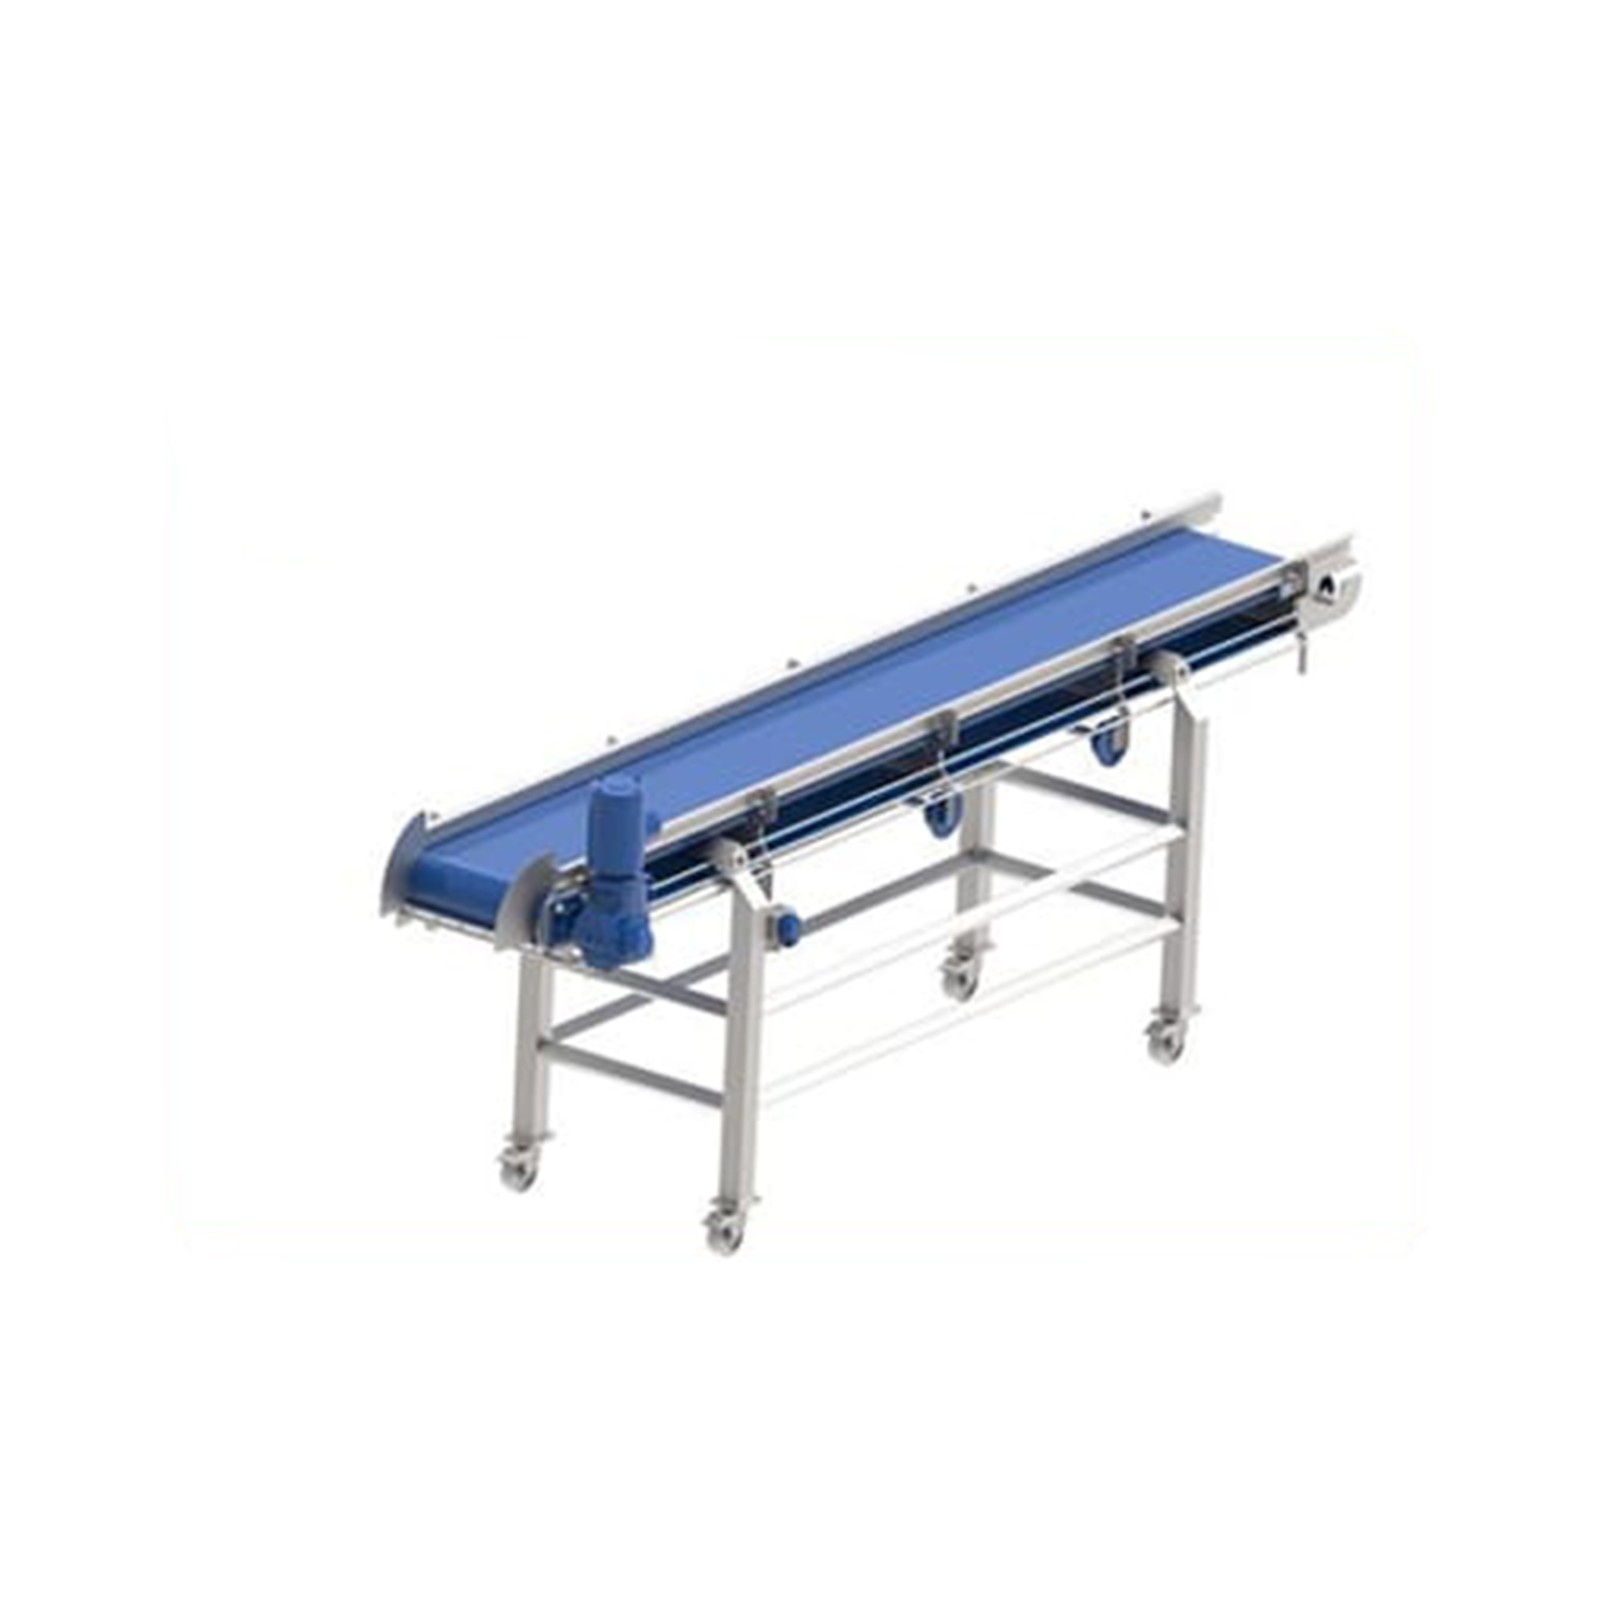
MODULAR BELT CONVEYOR
Modular Belt Conveyor offers robust, wear-resistant transport for diverse applications, including food, high-temperature, and chemical environments.
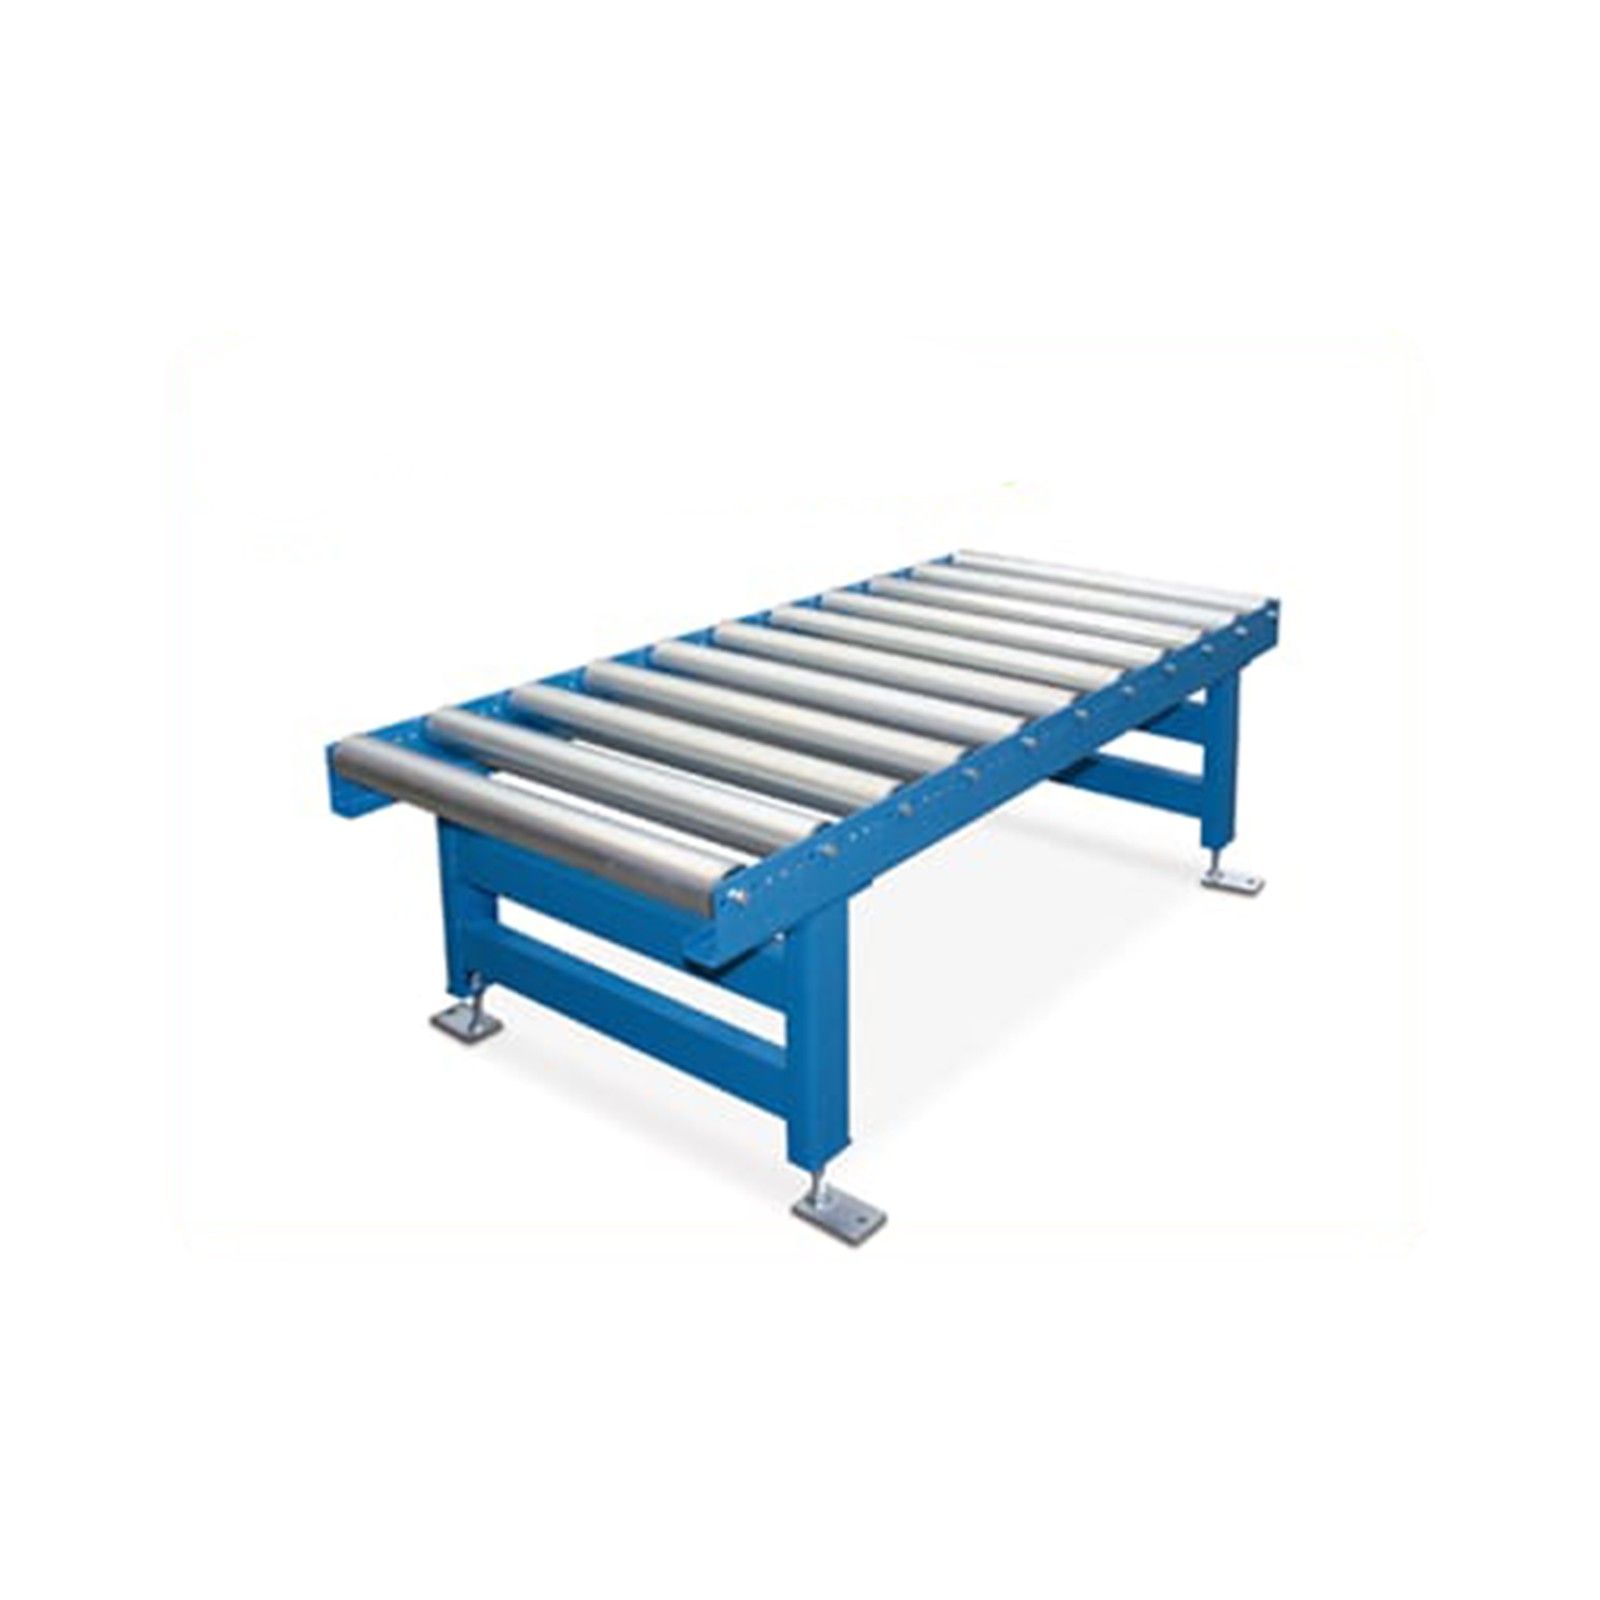
ROLLER CONVEYOR
Roller conveyors efficiently transport materials using rotating rollers powered by gravity or small motors.
PU BELT CONVEYOR
PU belt conveyors efficiently transport packaged and unpackaged goods of various shapes and sizes across industrial applications.
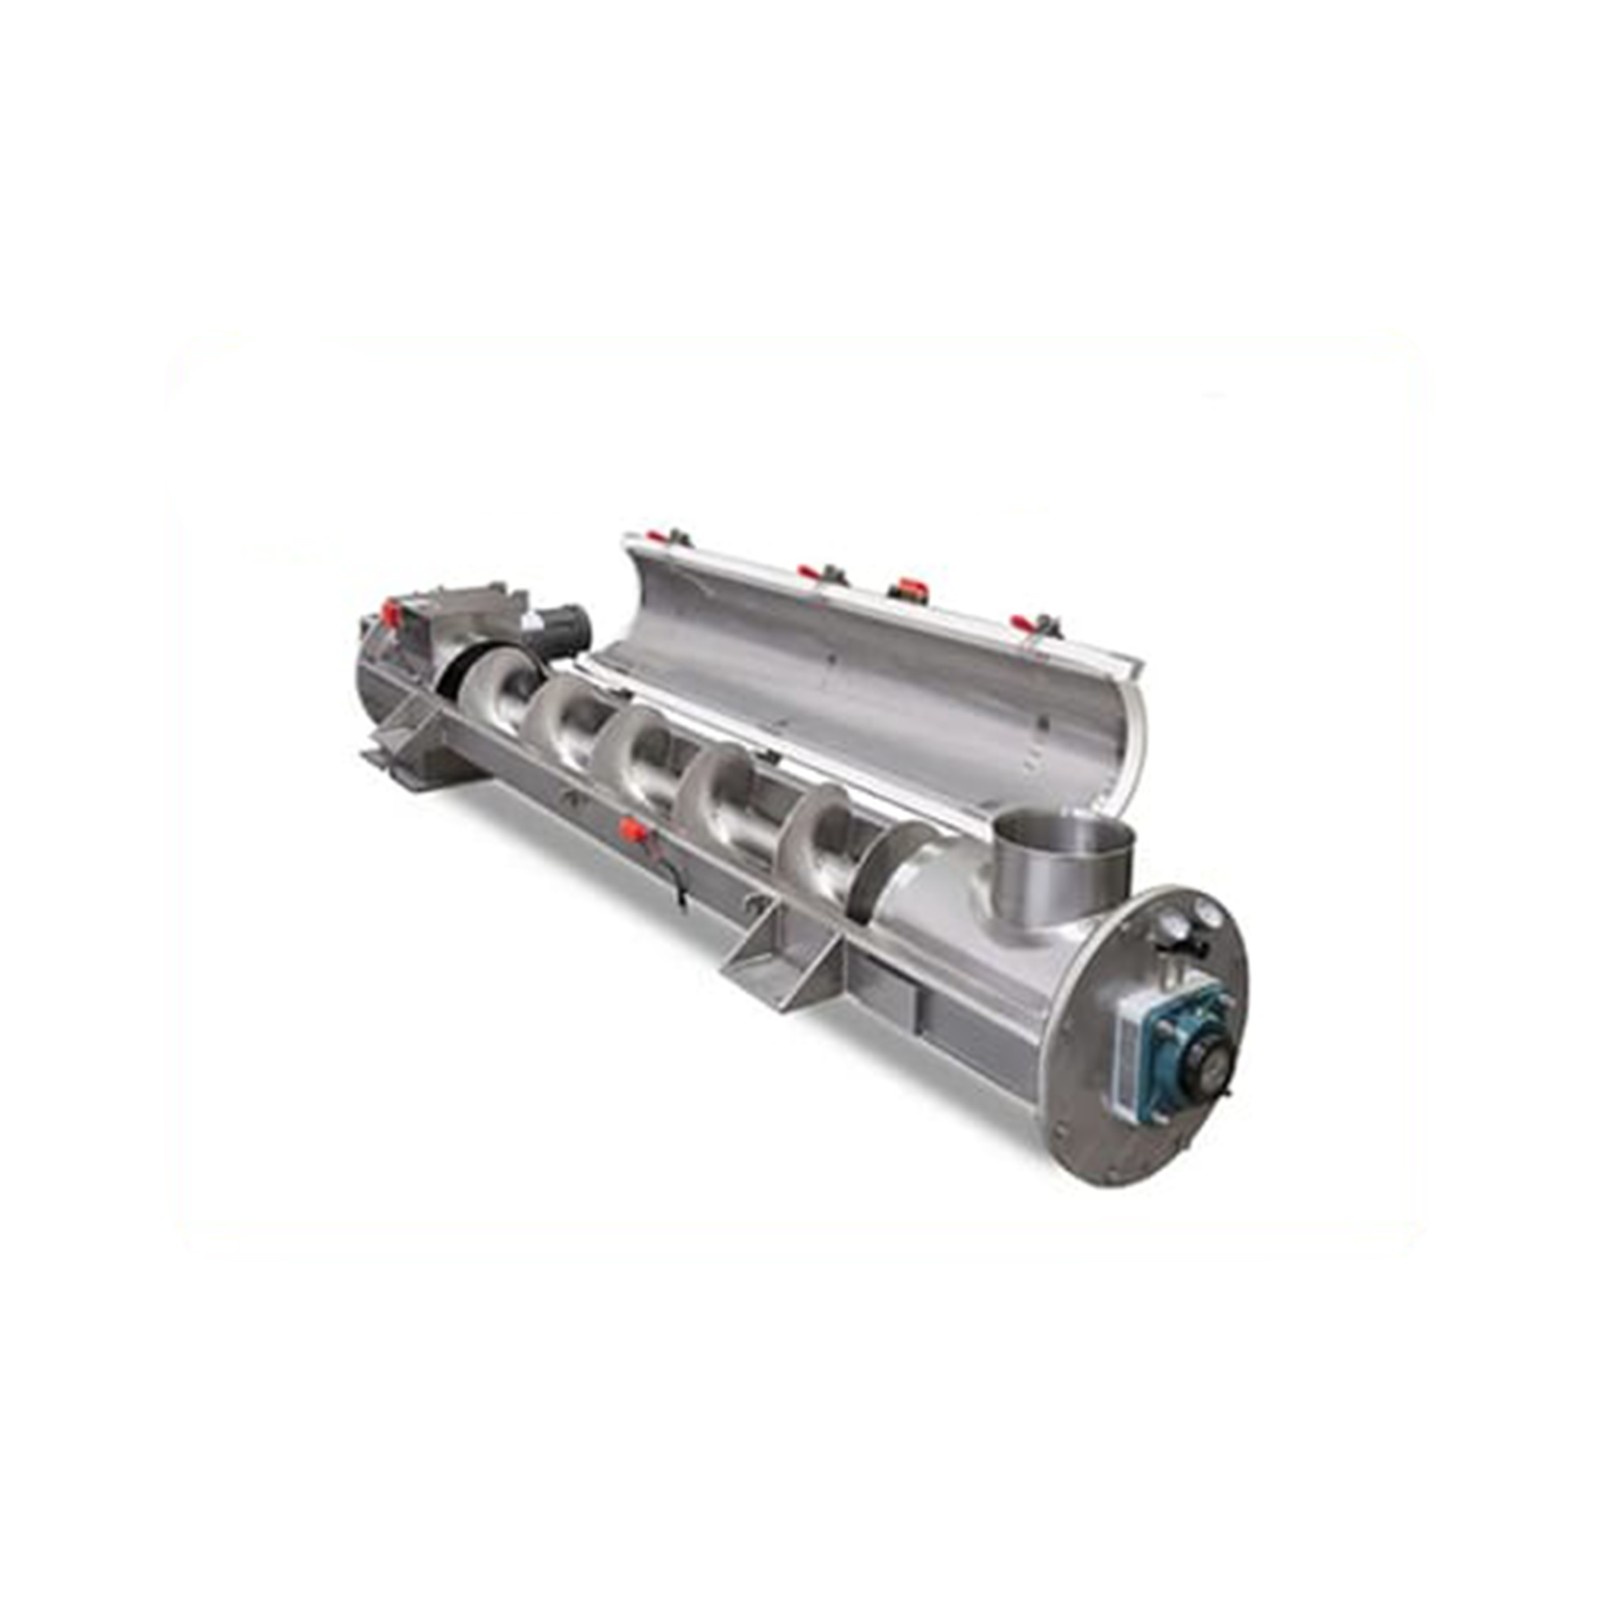
SCREW CONVEYOR
Screw conveyors efficiently transport granular and powdered materials horizontally or vertically across various industries.
FOOD GRADE CONVEYOR
Food-grade conveyors safely and efficiently transport food products using hygienic, reliable conveyor systems.
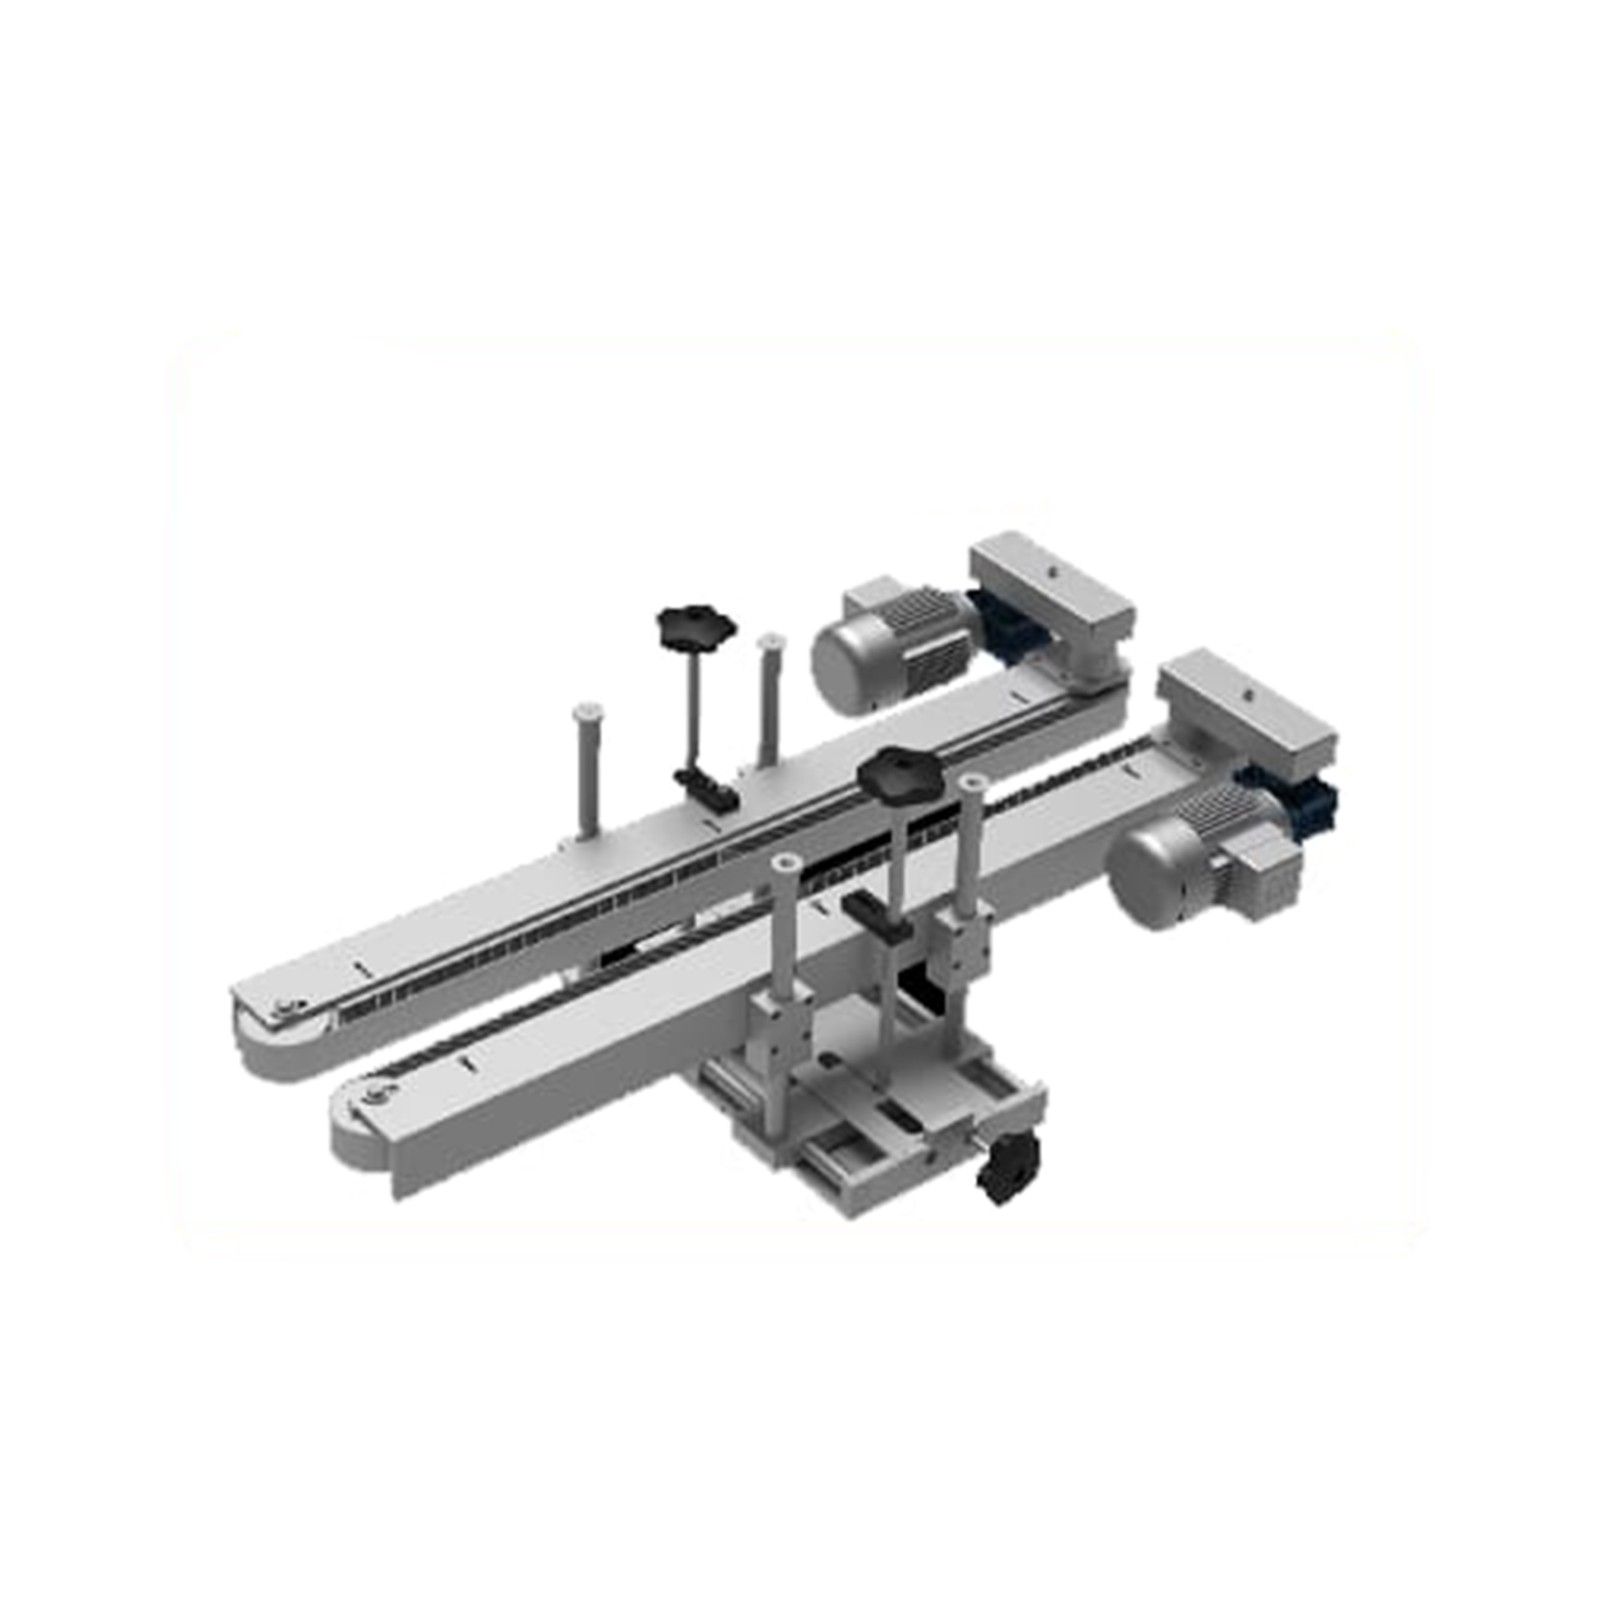
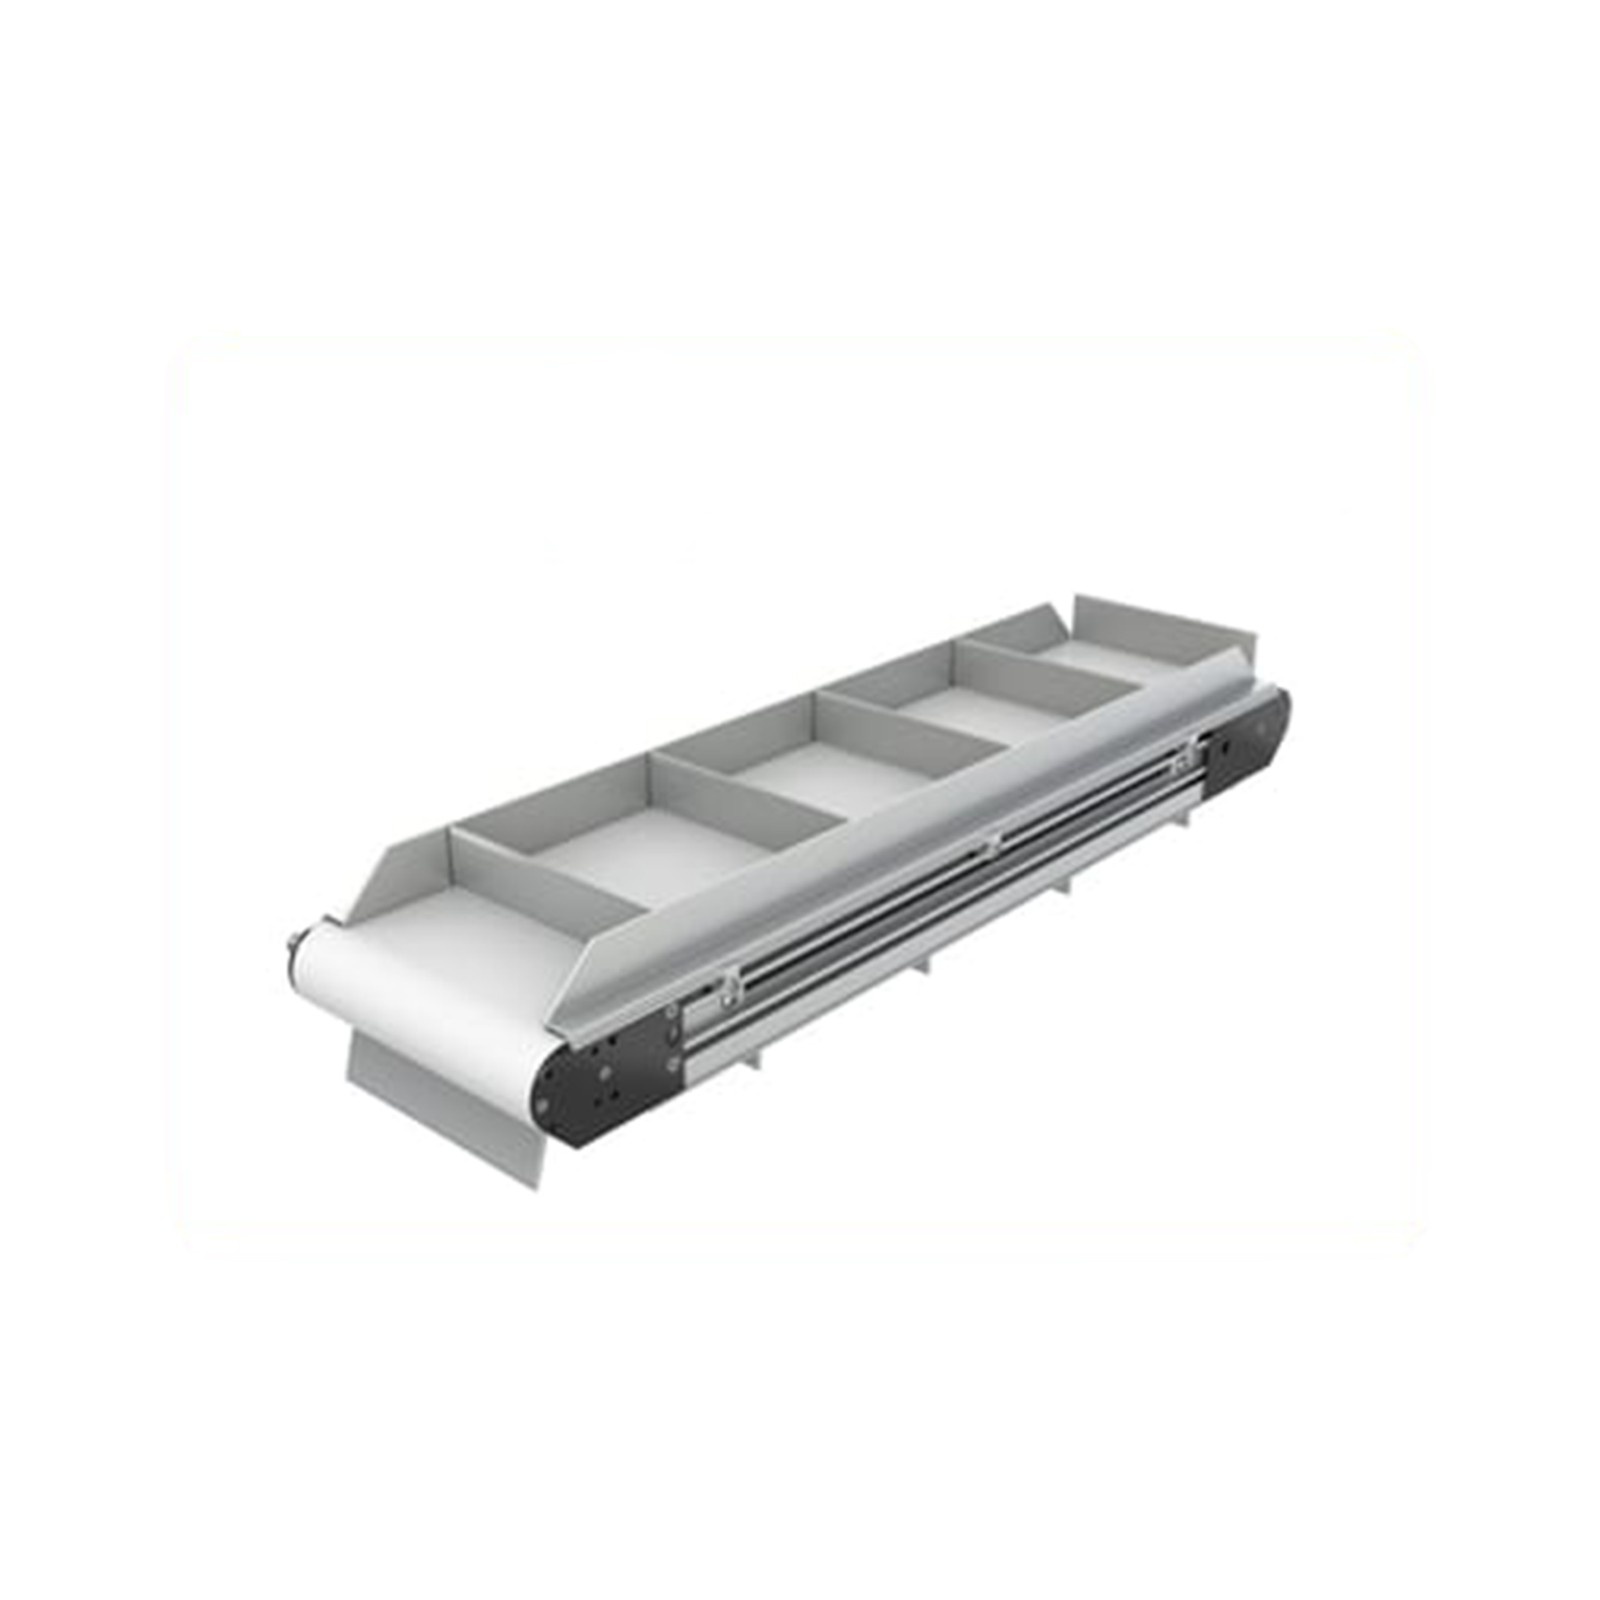
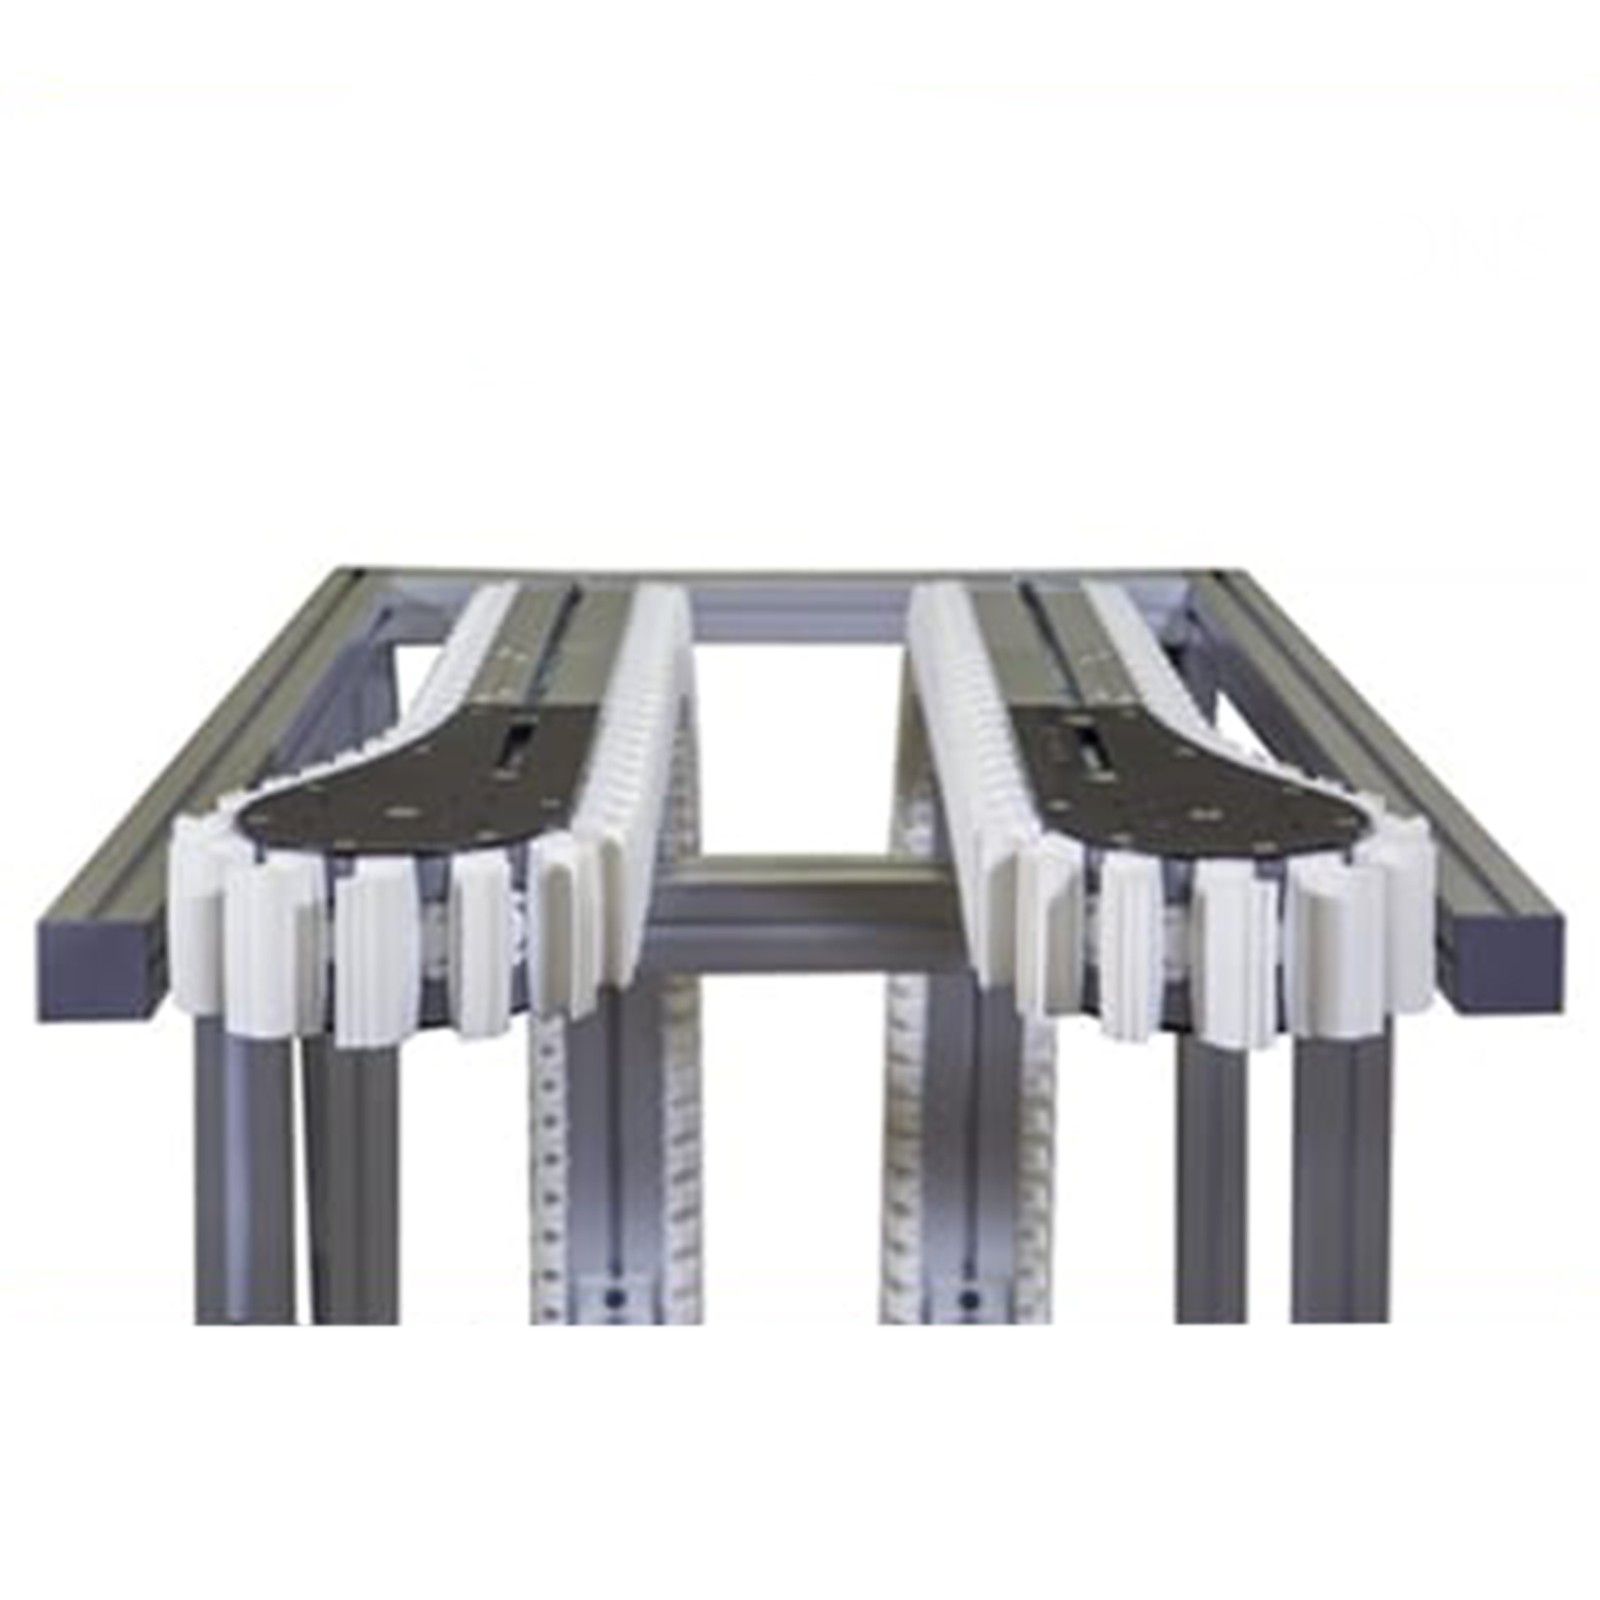
WEDGE CONVEYOR
Wedge conveyors use parallel belts with adjustable widths for flexible and secure product transport.
SIDE GRIP CONVEYORs
Side grip conveyors securely hold products from the sides, enabling reliable transport on steep inclines while keeping the top and bottom accessible.
RETRACTING CONVEYOR
Retracting conveyors provide flexible material handling with manually or pneumatically adjustable frames for precise and efficient product transfer.
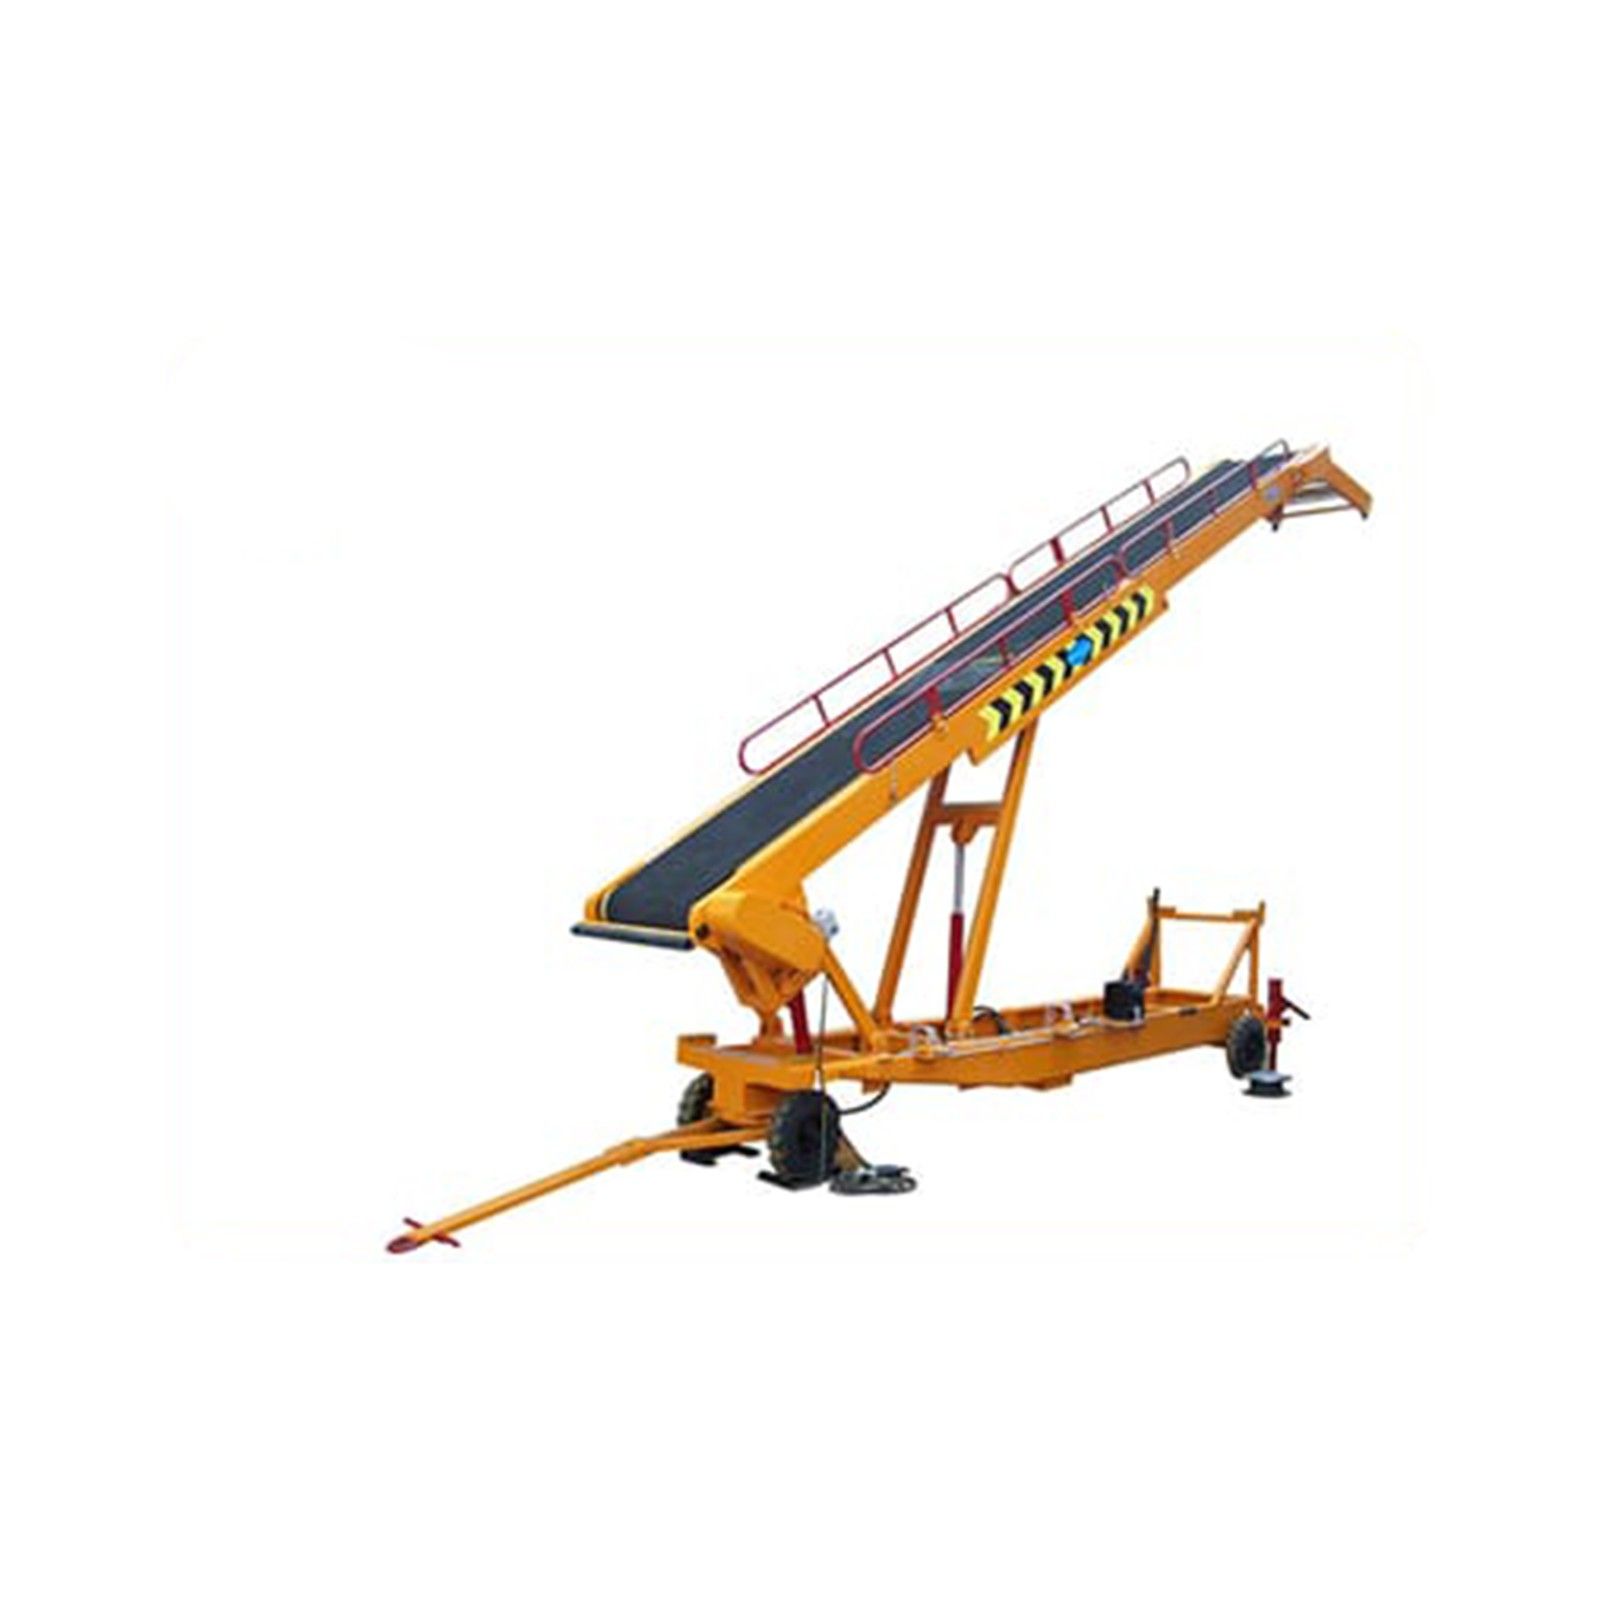
LOADING / UNLOADING CONVEYOR
Loading and unloading conveyors enable fast, efficient material handling for boxes, cartons, and bags while reducing labor and saving time.
FLAT BELT CONVEYOR
Flat belt conveyors provide reliable material transport with easy belt alignment and adjustment for efficient operation.
BULK MATERIAL CONVEYOR
Bulk material conveyors efficiently transport large quantities of loose materials such as powders, grains, and other bulk products.
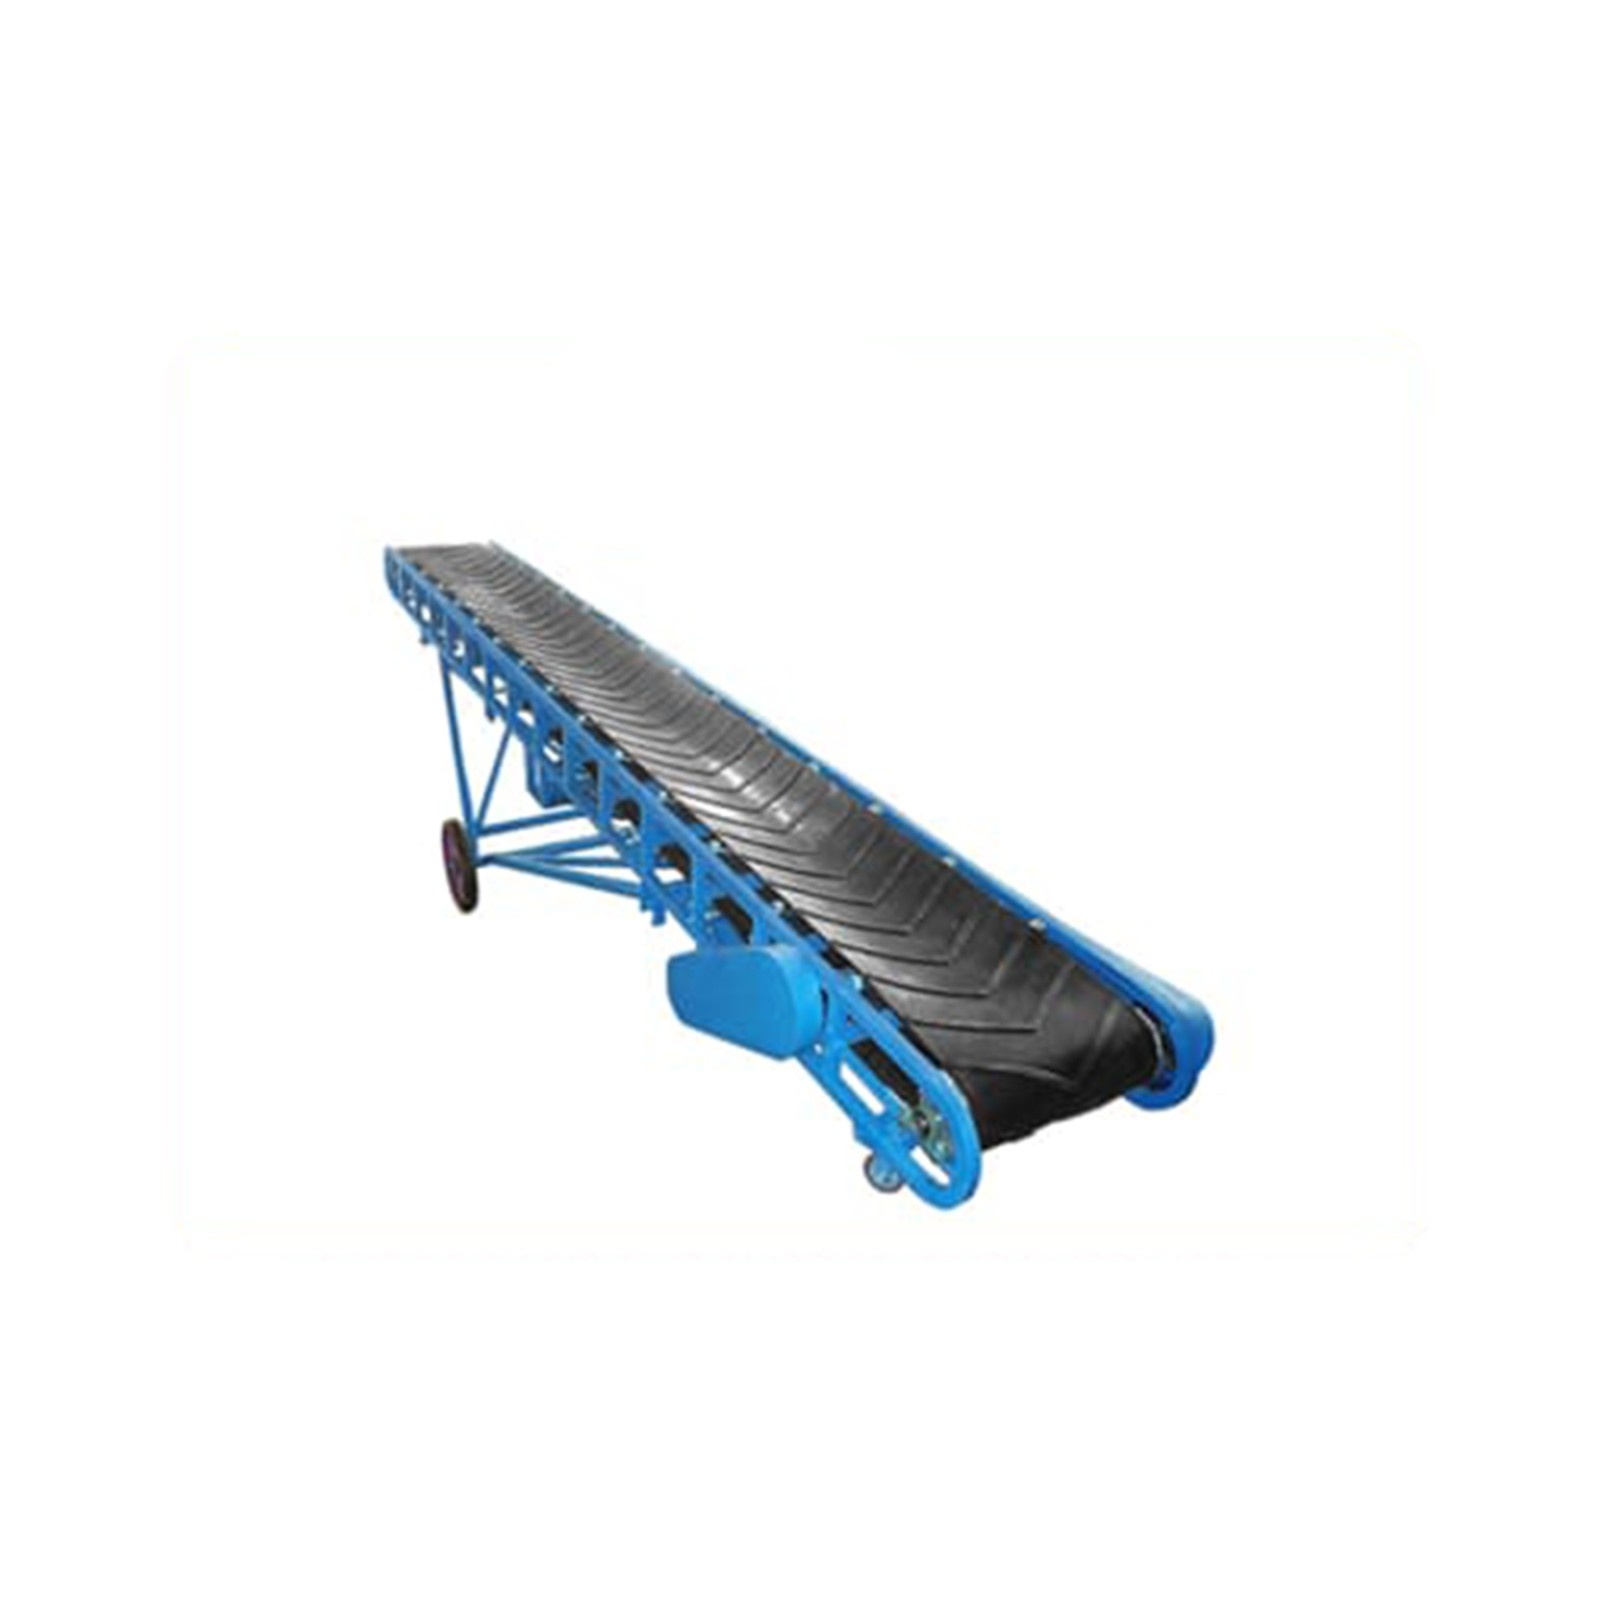
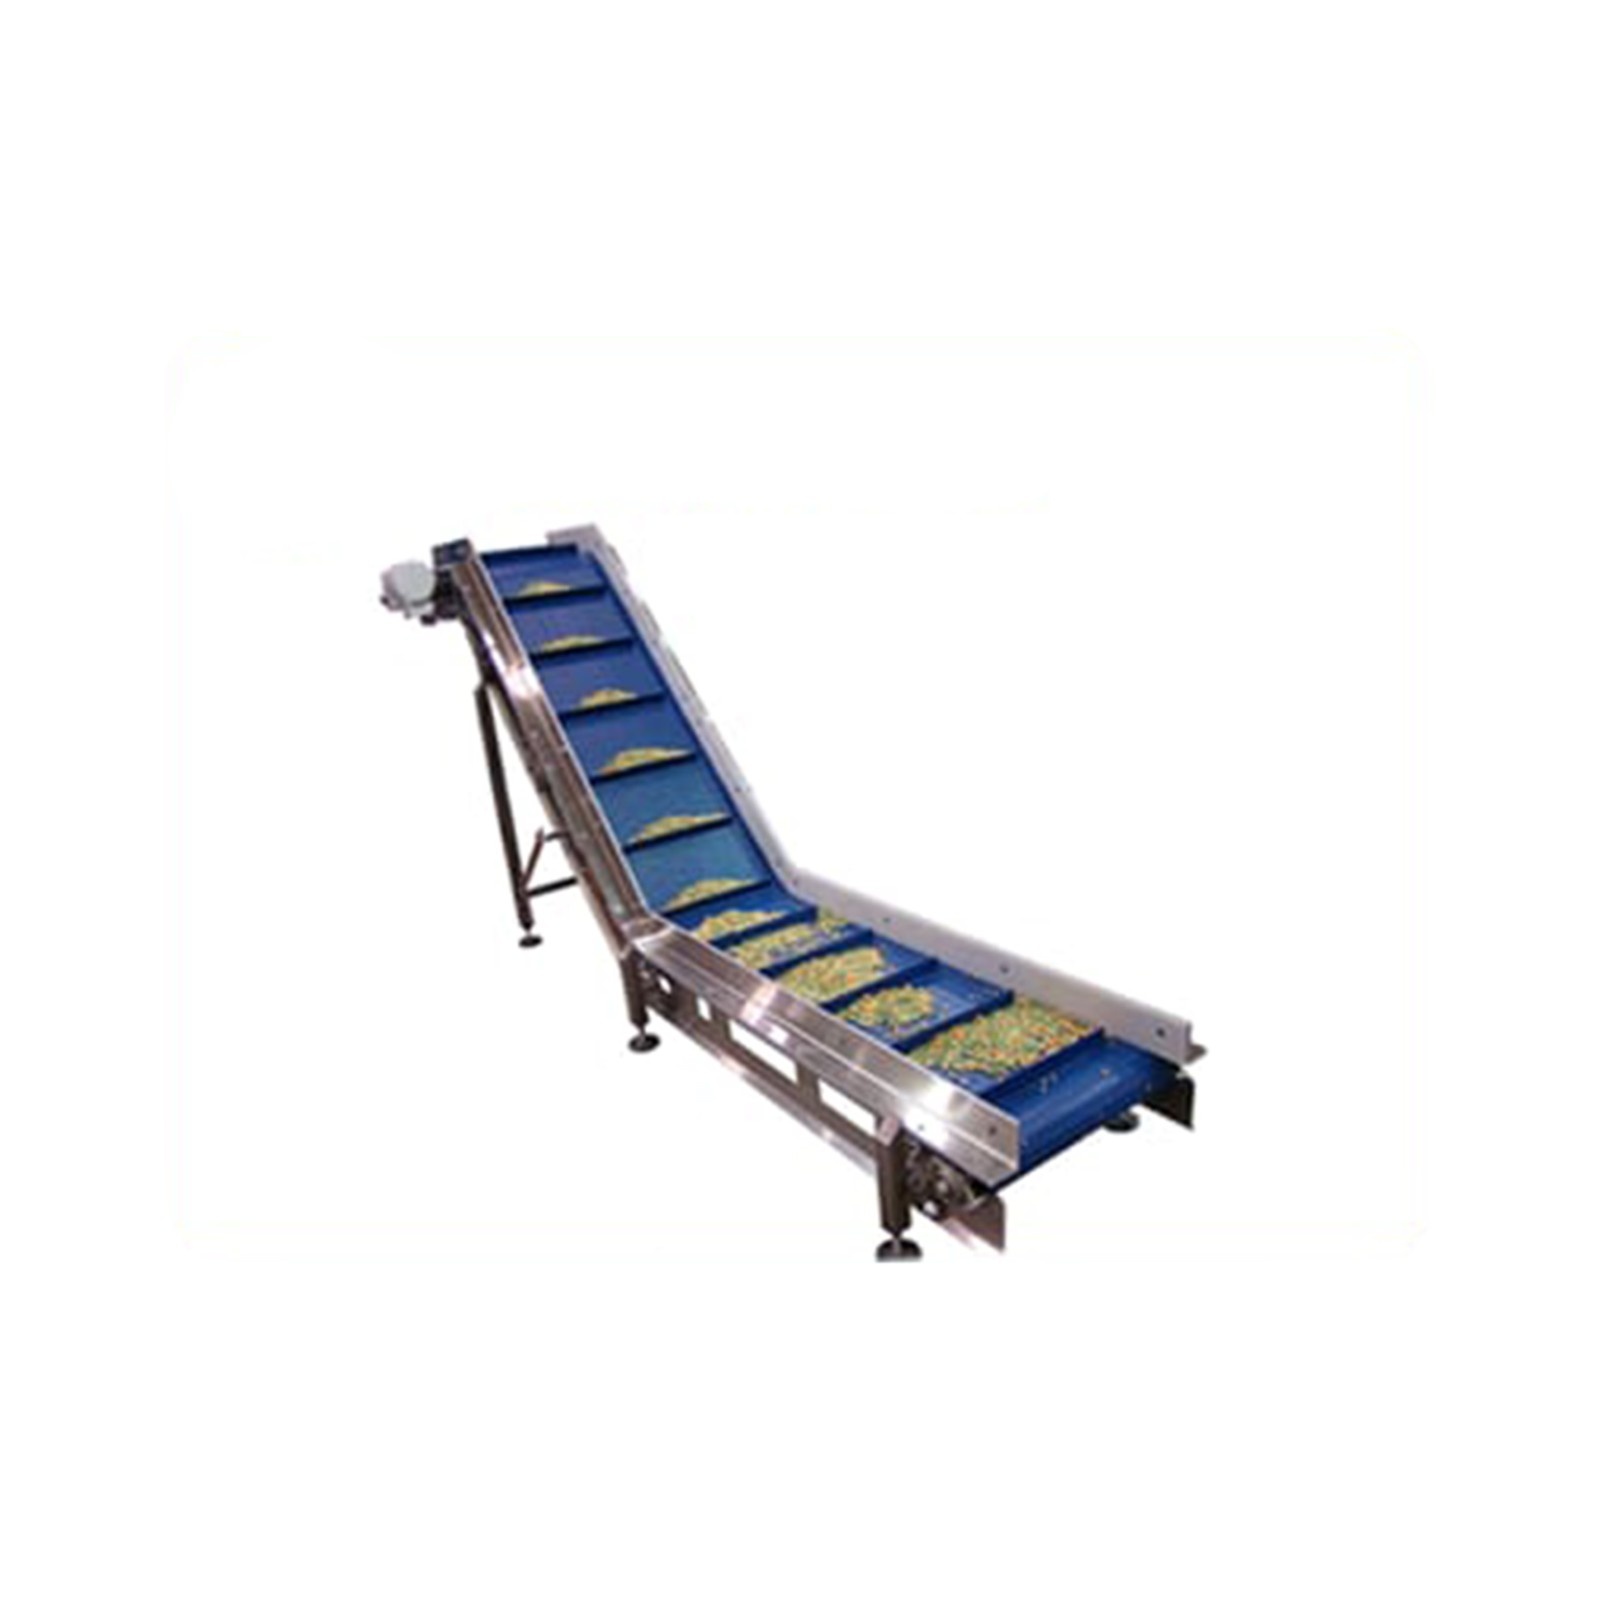
CLEATED BELT CONVEYOR
Cleated belt conveyors efficiently move products on inclines, maintain spacing, and support reliable product staging in manufacturing applications.
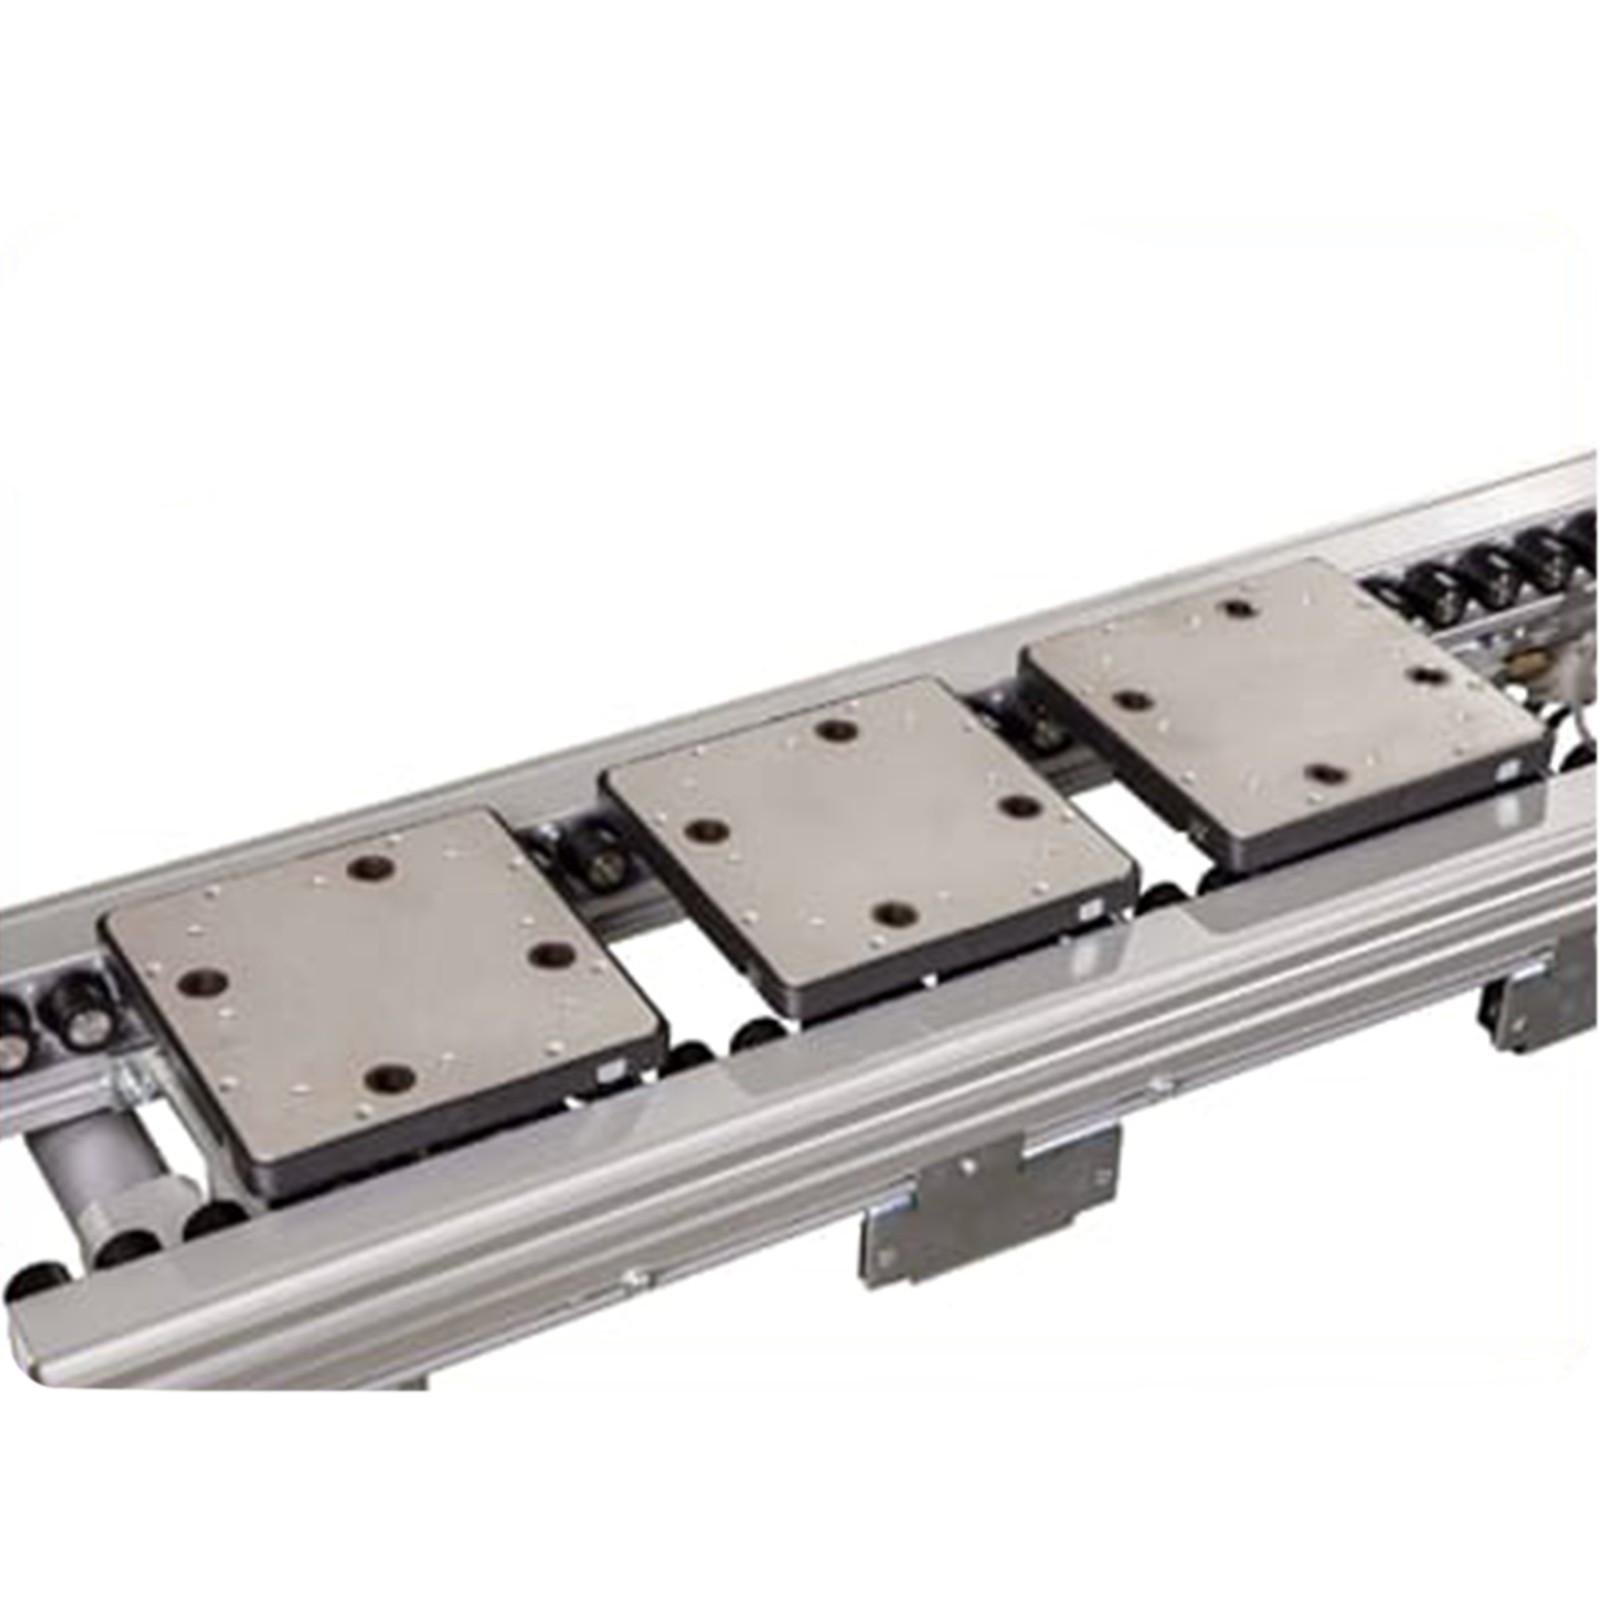
PALLET CONVEYOR
Pallet conveyors efficiently transport products on pallets using belts, chains, or powered rollers for reliable material handling.
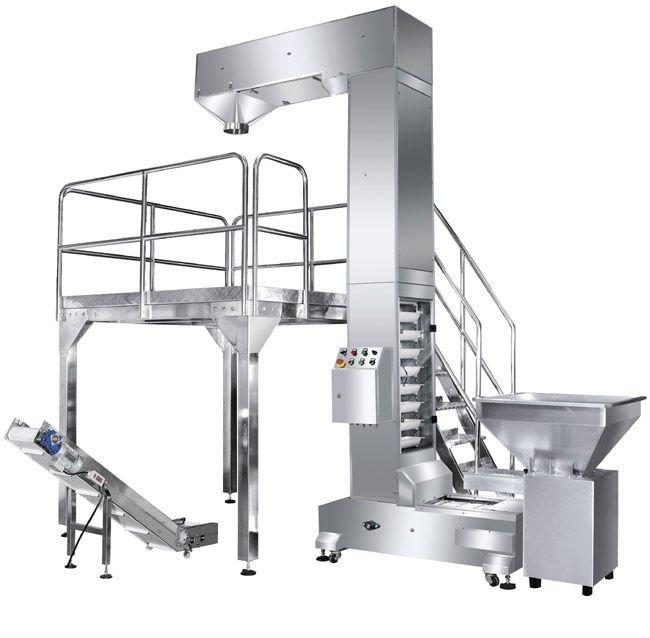
BUCKET ELEVATOR
Bucket elevators efficiently transport bulk materials vertically using buckets attached to a rotating belt or chain.
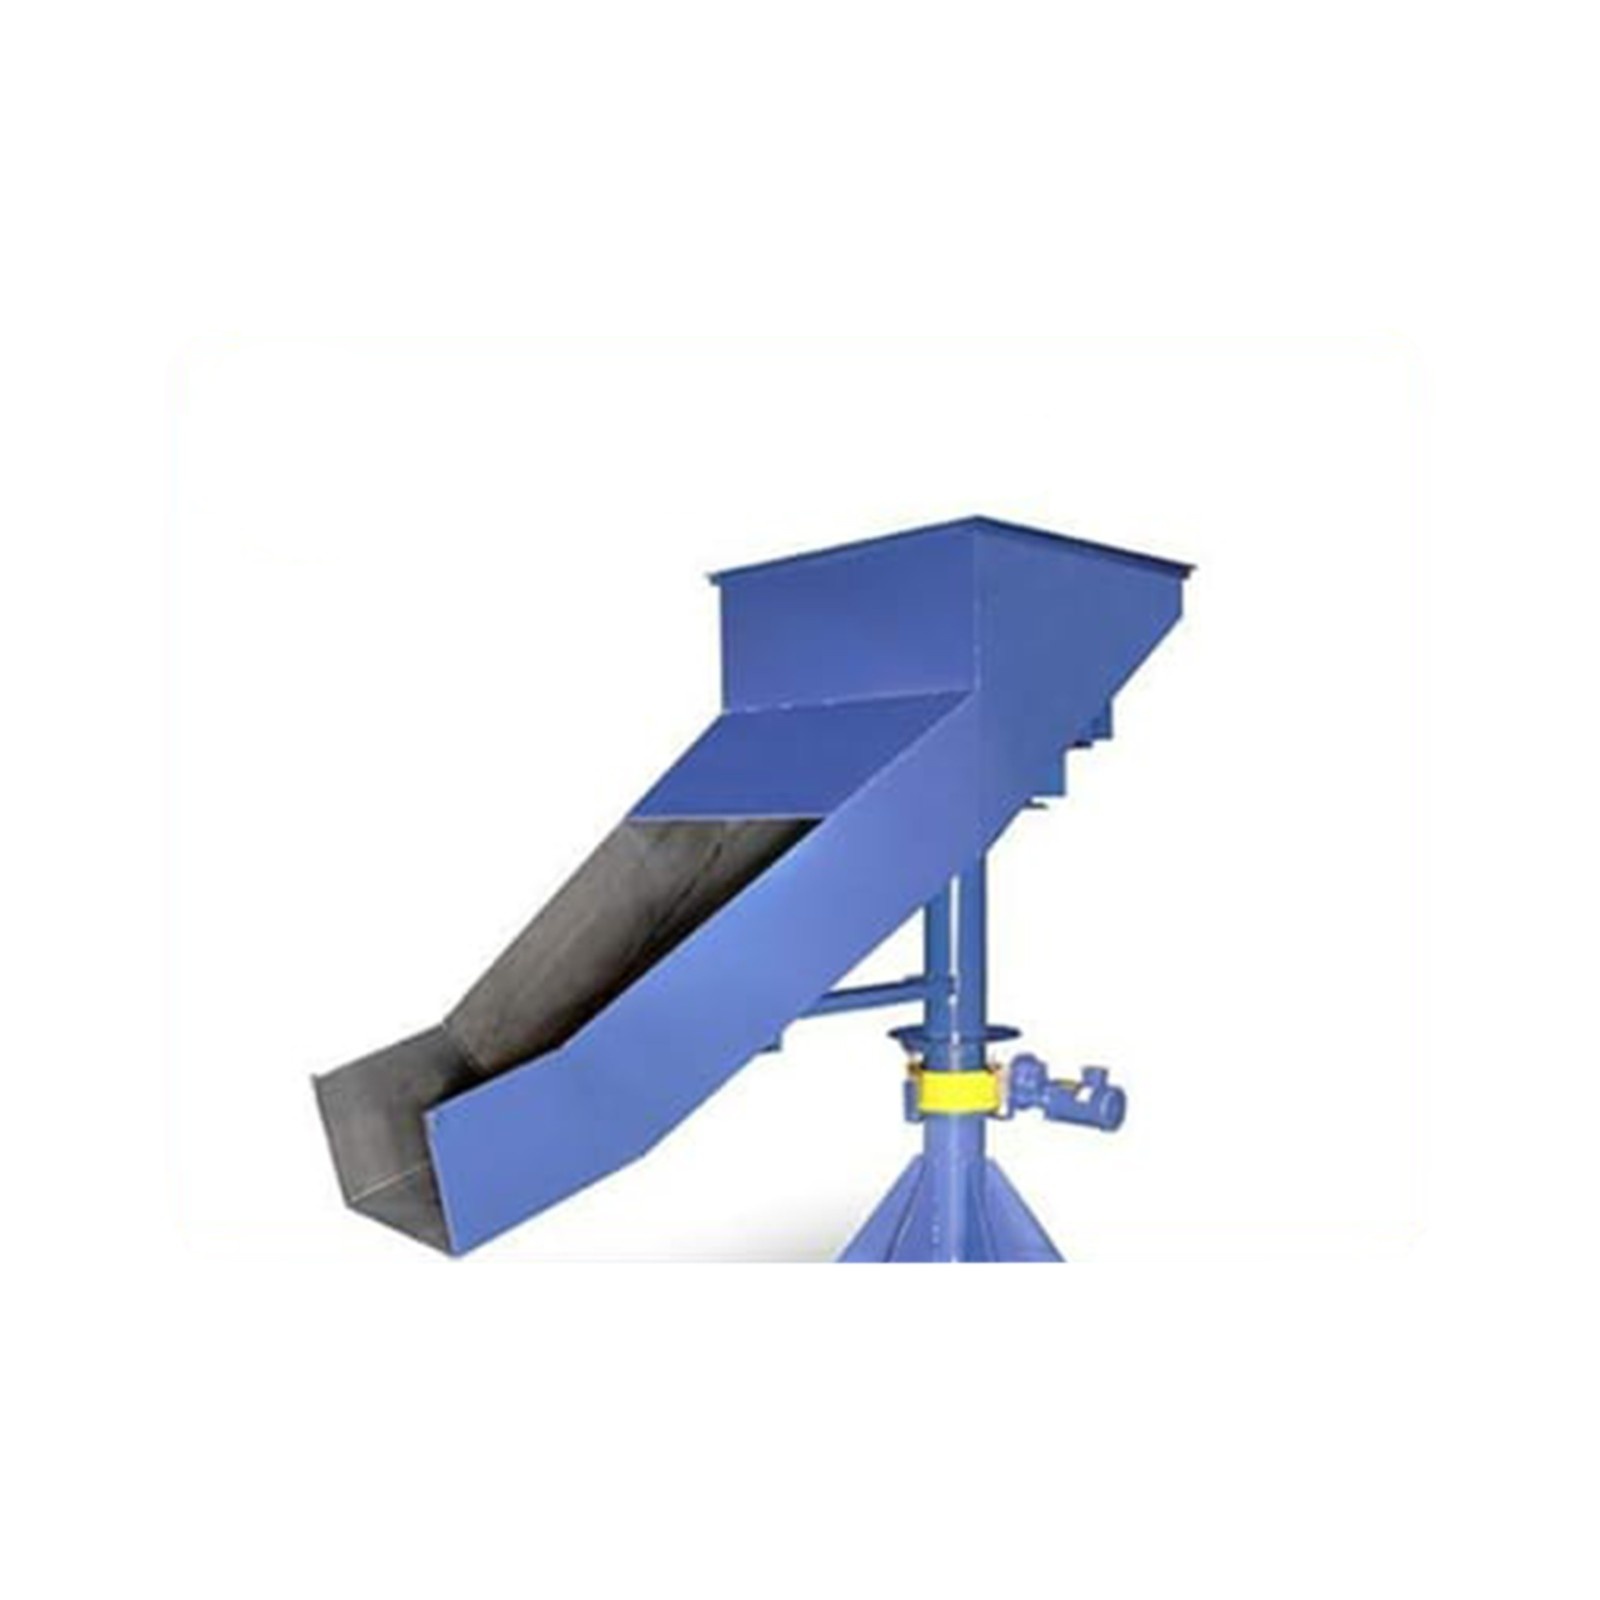
TROUGH CONVEYOR
Trough conveyors efficiently transport loose and bulk materials while keeping them centered, making them ideal for abrasive materials.
SLAT CHAIN CONVEYOR
Slat chain conveyors use motor-driven chains and slats to efficiently transport products from one point to another.
FLEXIBLE CONVEYOR
Flexible conveyors easily roll and curve to adapt to different discharge points, making them ideal for loading docks and truck trailers.
SPIRAL CONVEYOR
Spiral conveyors provide compact, smooth, and reliable vertical product transport between floors, machines, and work areas.
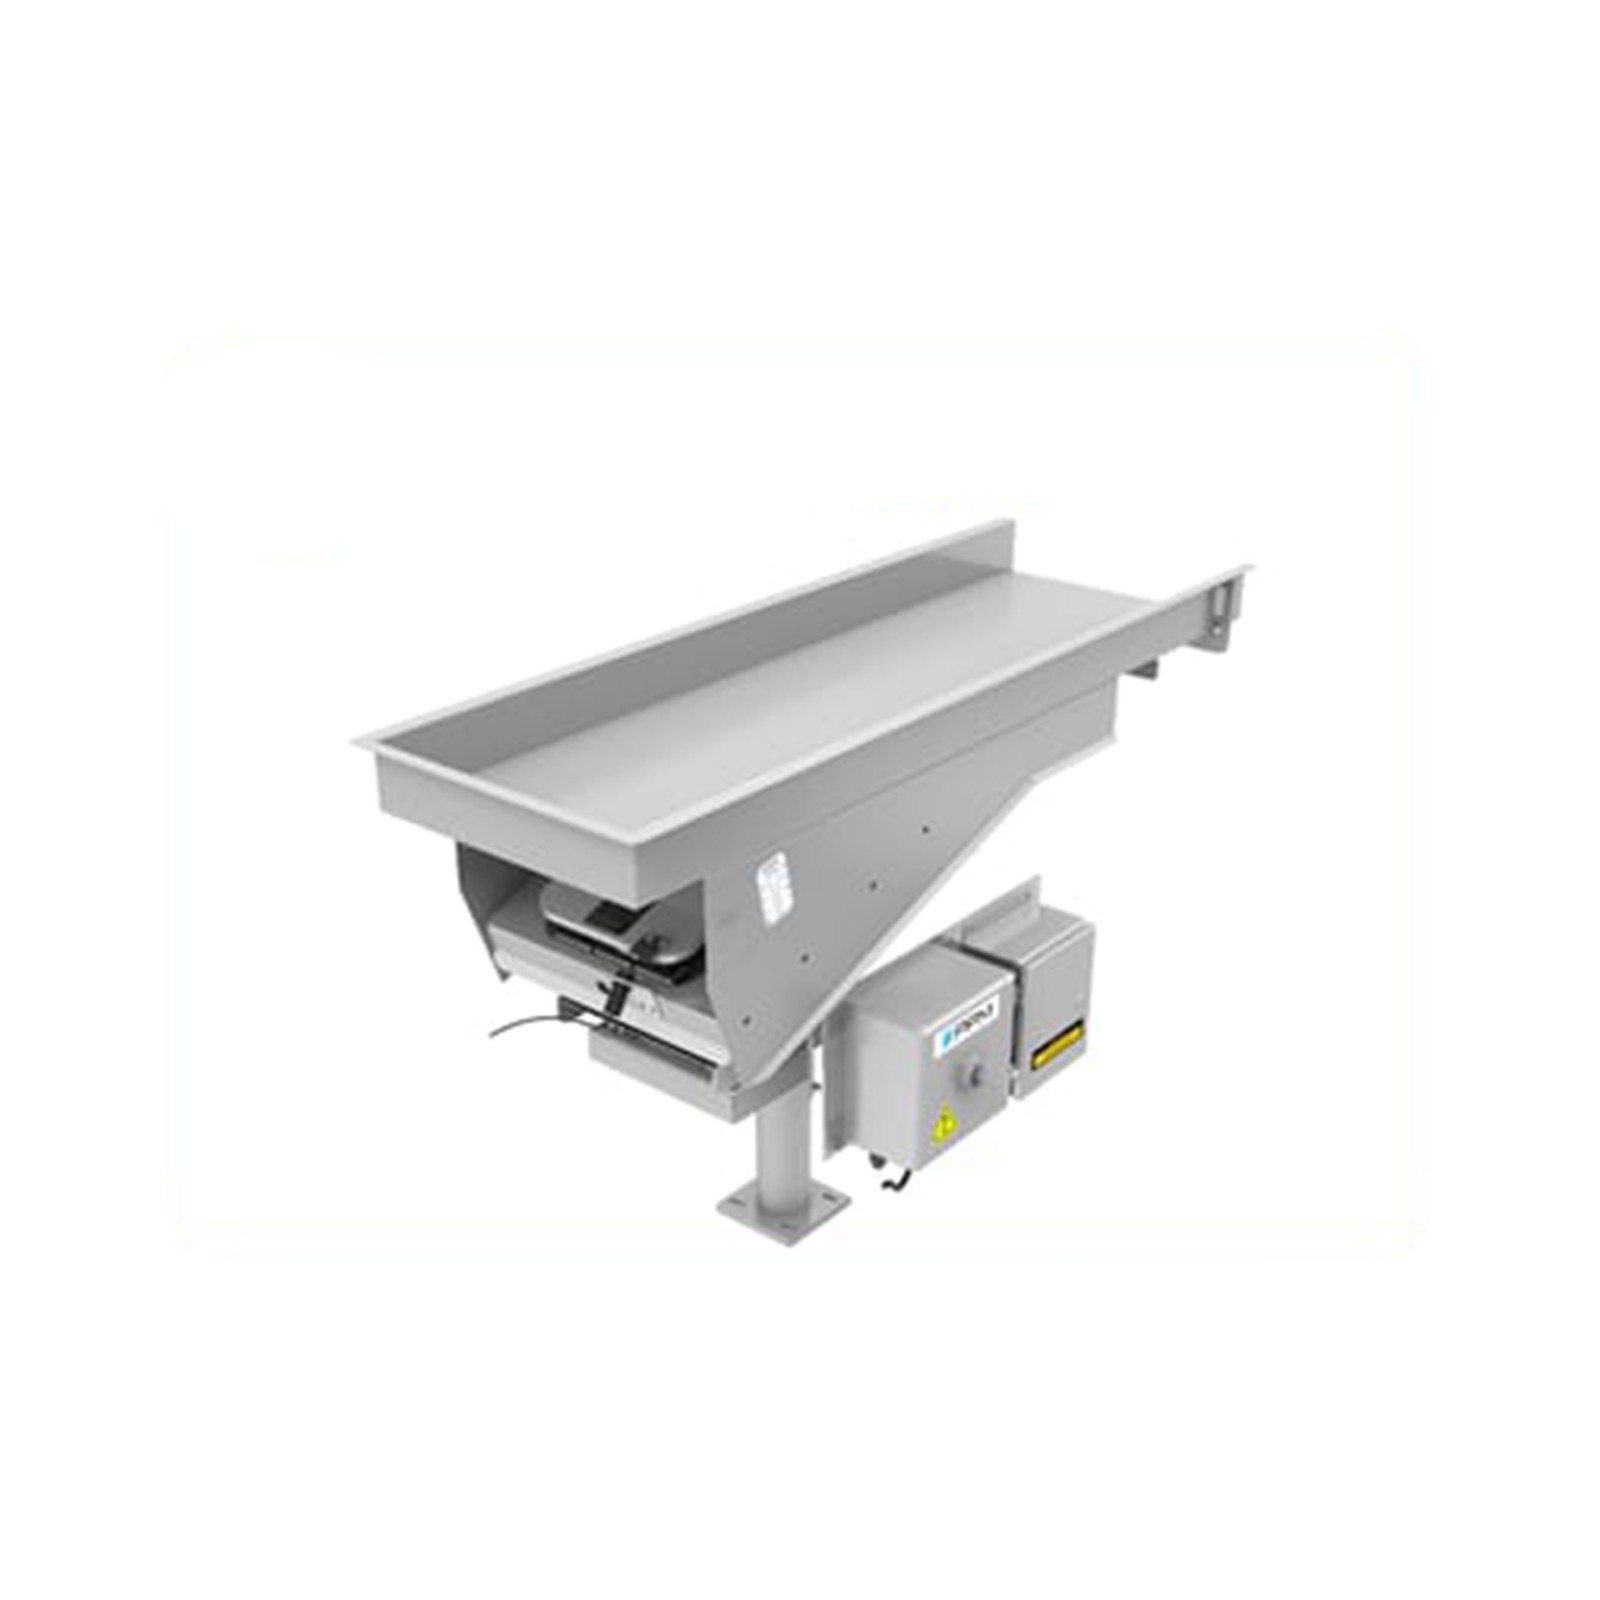
VIBRATING CONVEYOR
Vibrating conveyors use controlled vibration to efficiently move bulk materials and products in a smooth, directional flow.
CHUTE CONVEYOR
Chute conveyors provide a simple, cost-effective gravity solution for material handling, accumulation, and vertical movement between floors.
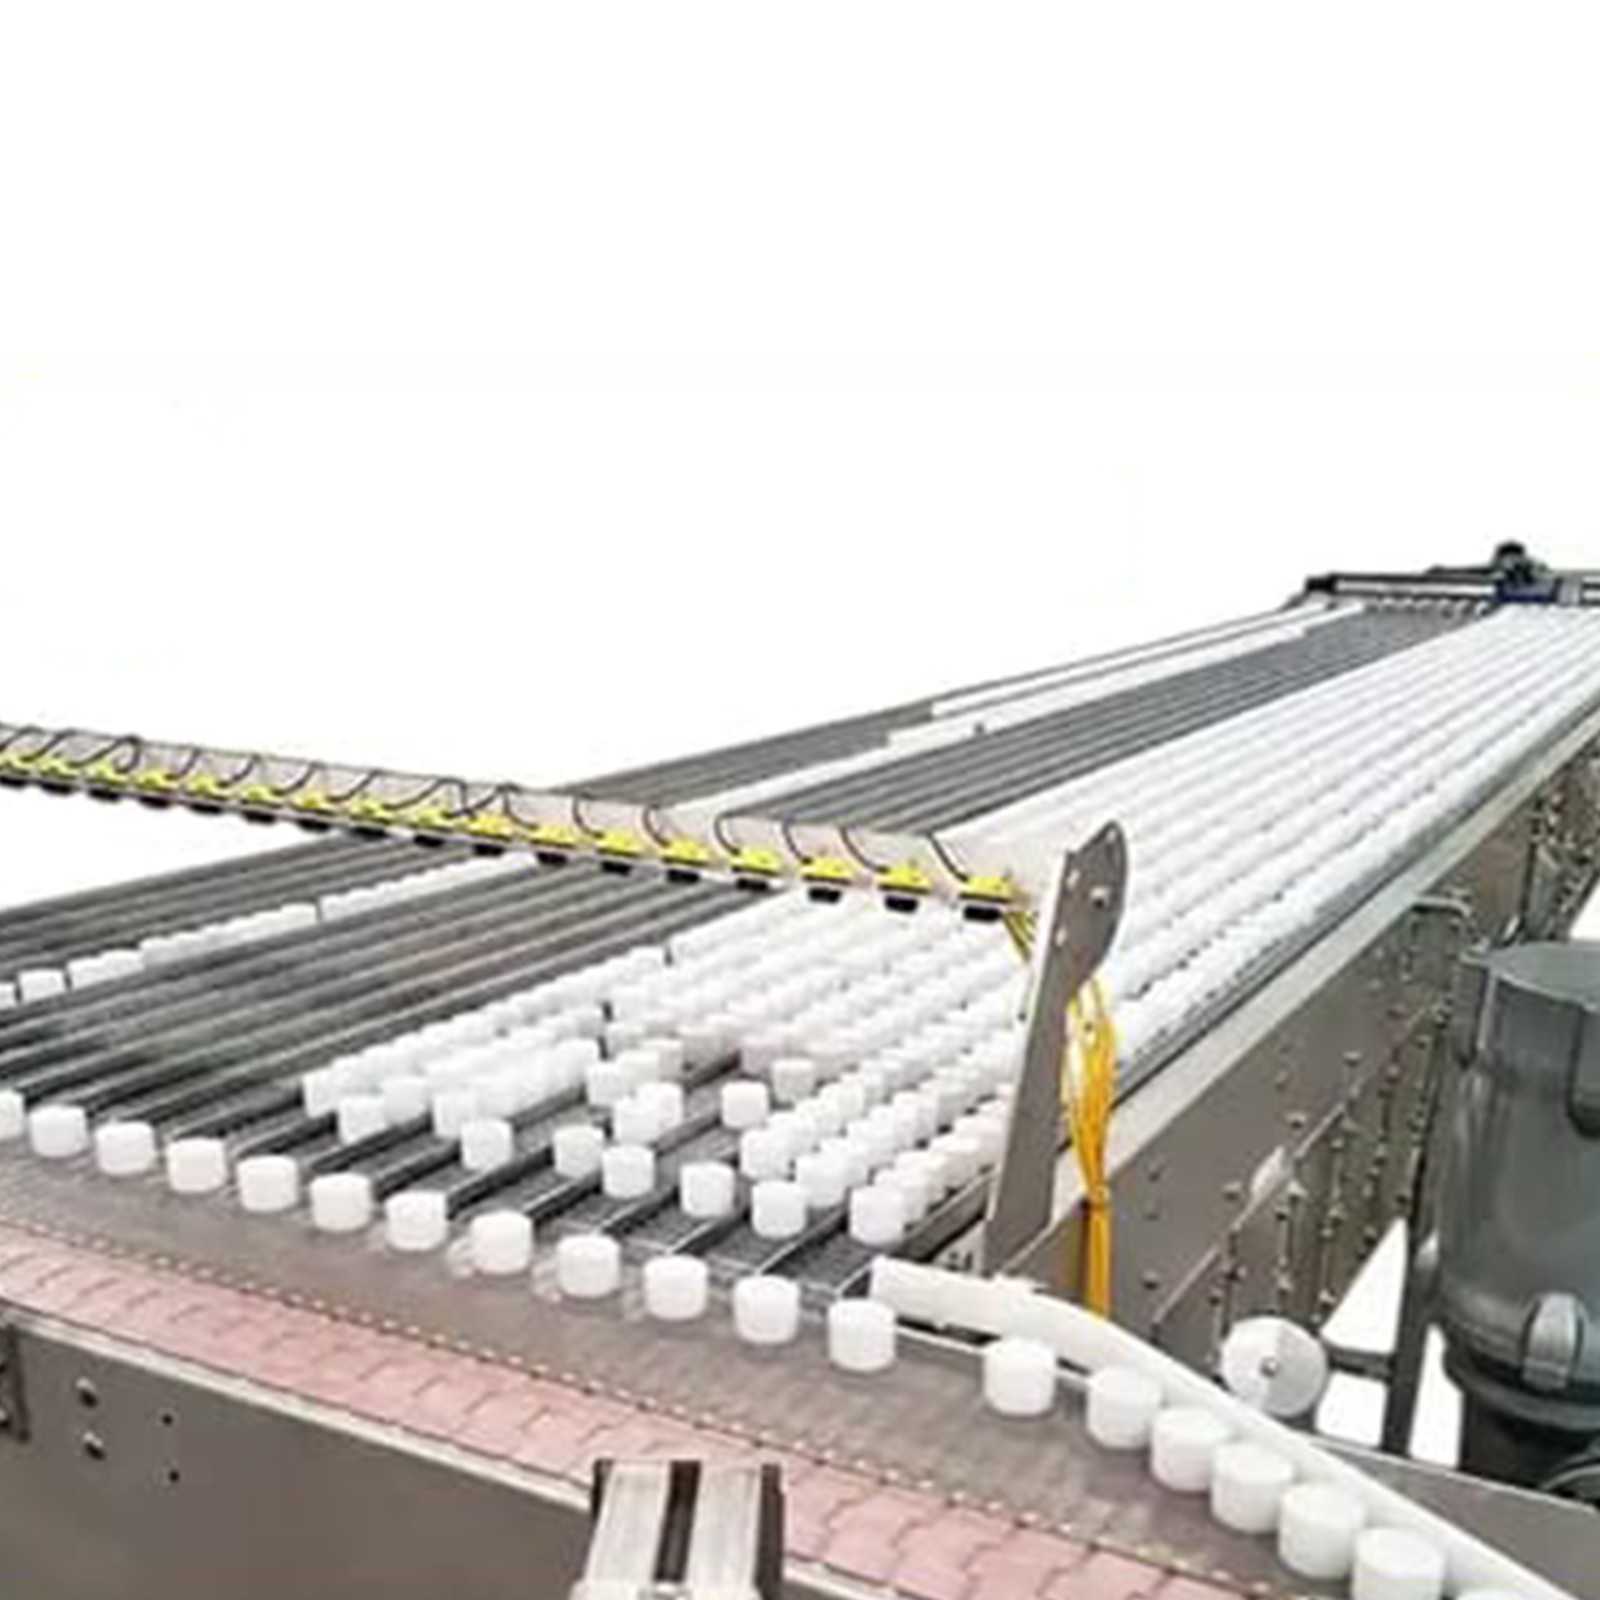
ACCUMULATION CONVEYOR
Accumulation conveyors temporarily hold and buffer products, supporting efficient picking, packing, and controlled material flow.
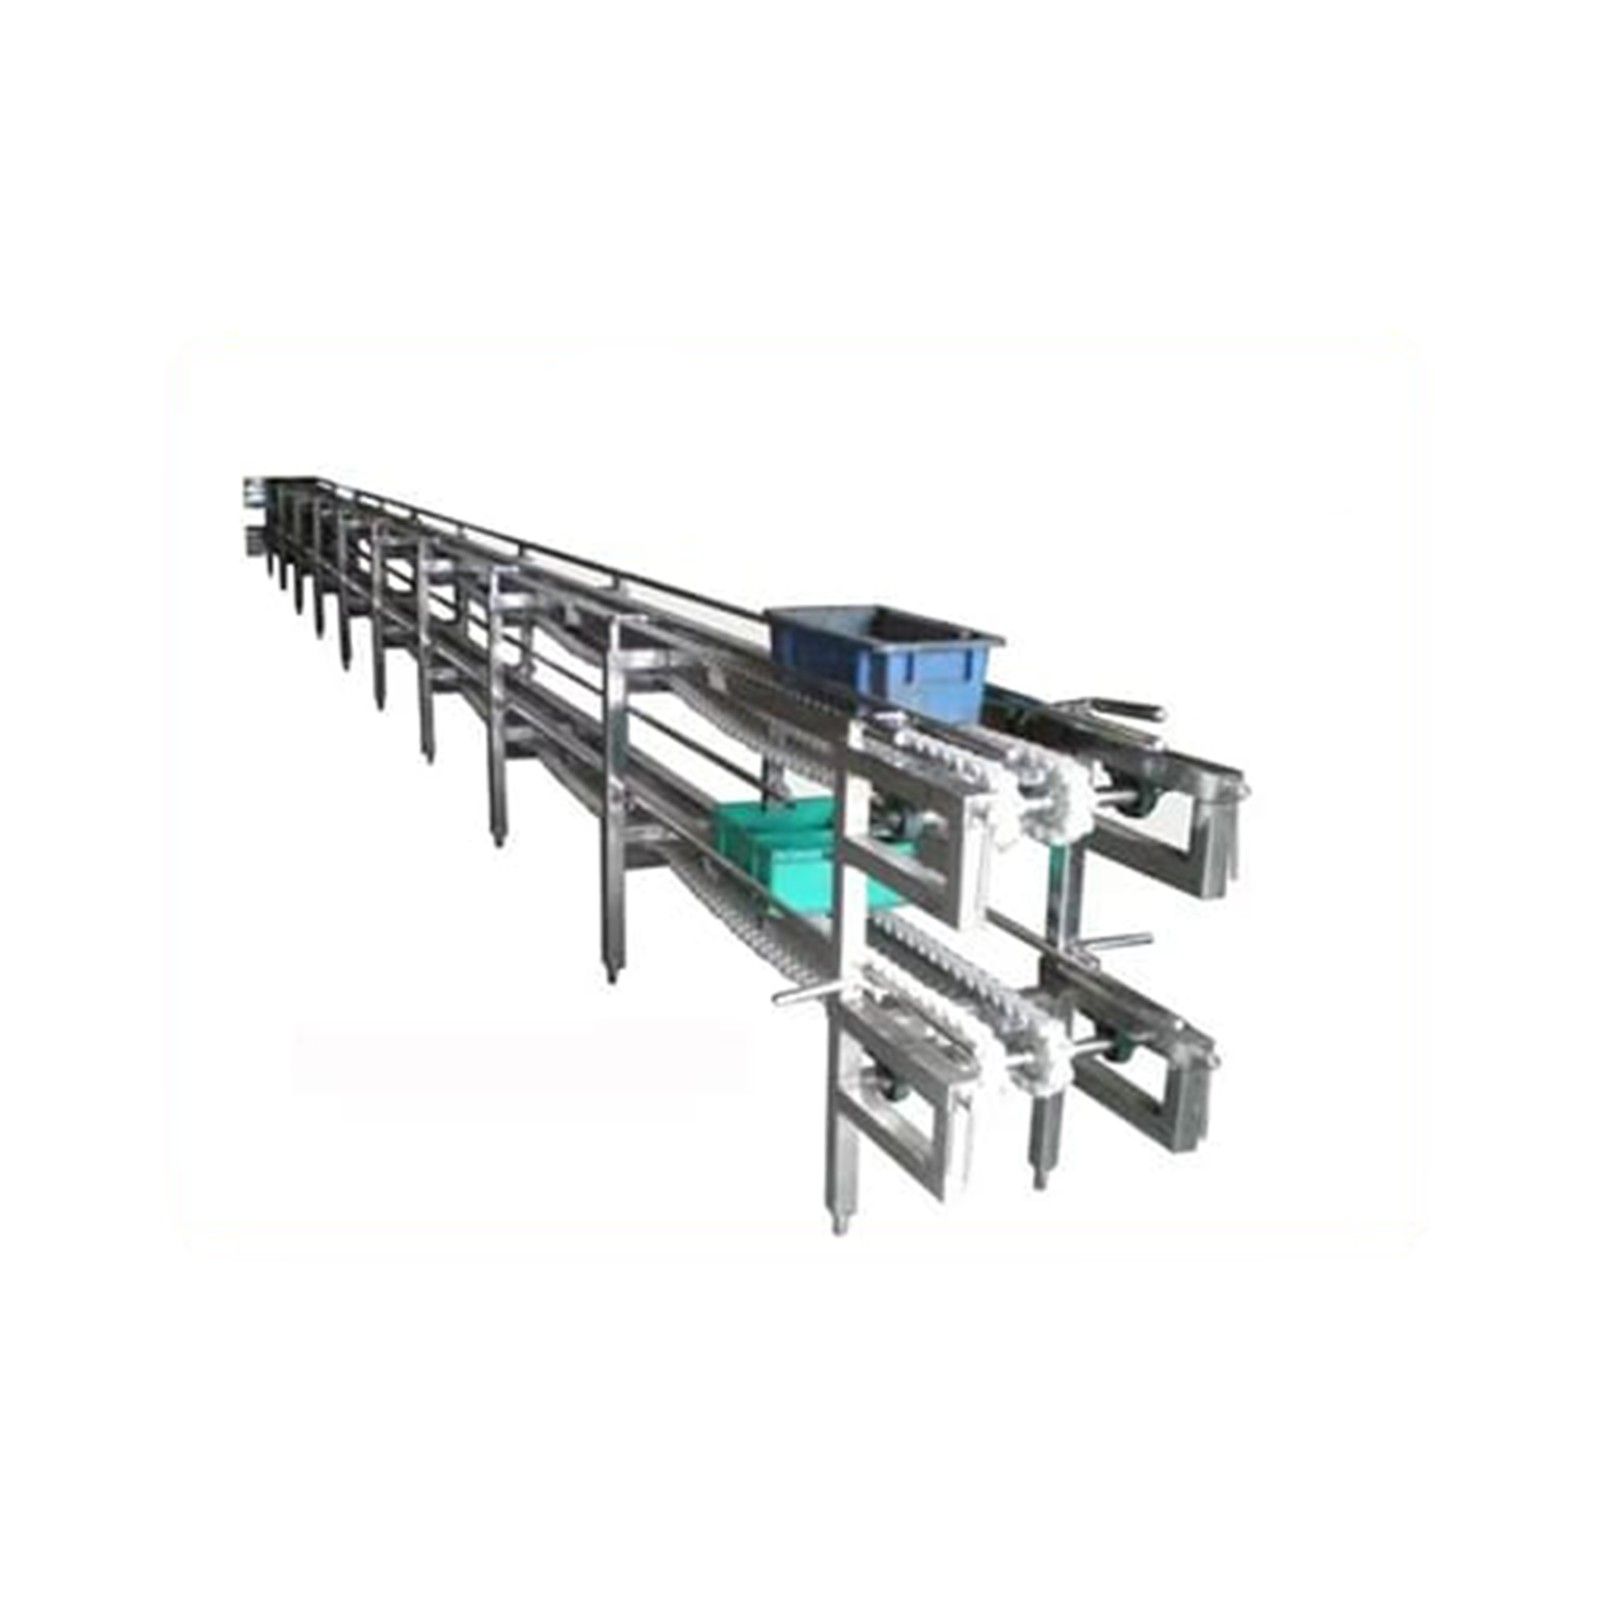
CRATE CONVEYOR
Crate conveyors efficiently transport carts and containers, making them ideal for multi-level retail stores and warehouse applications.
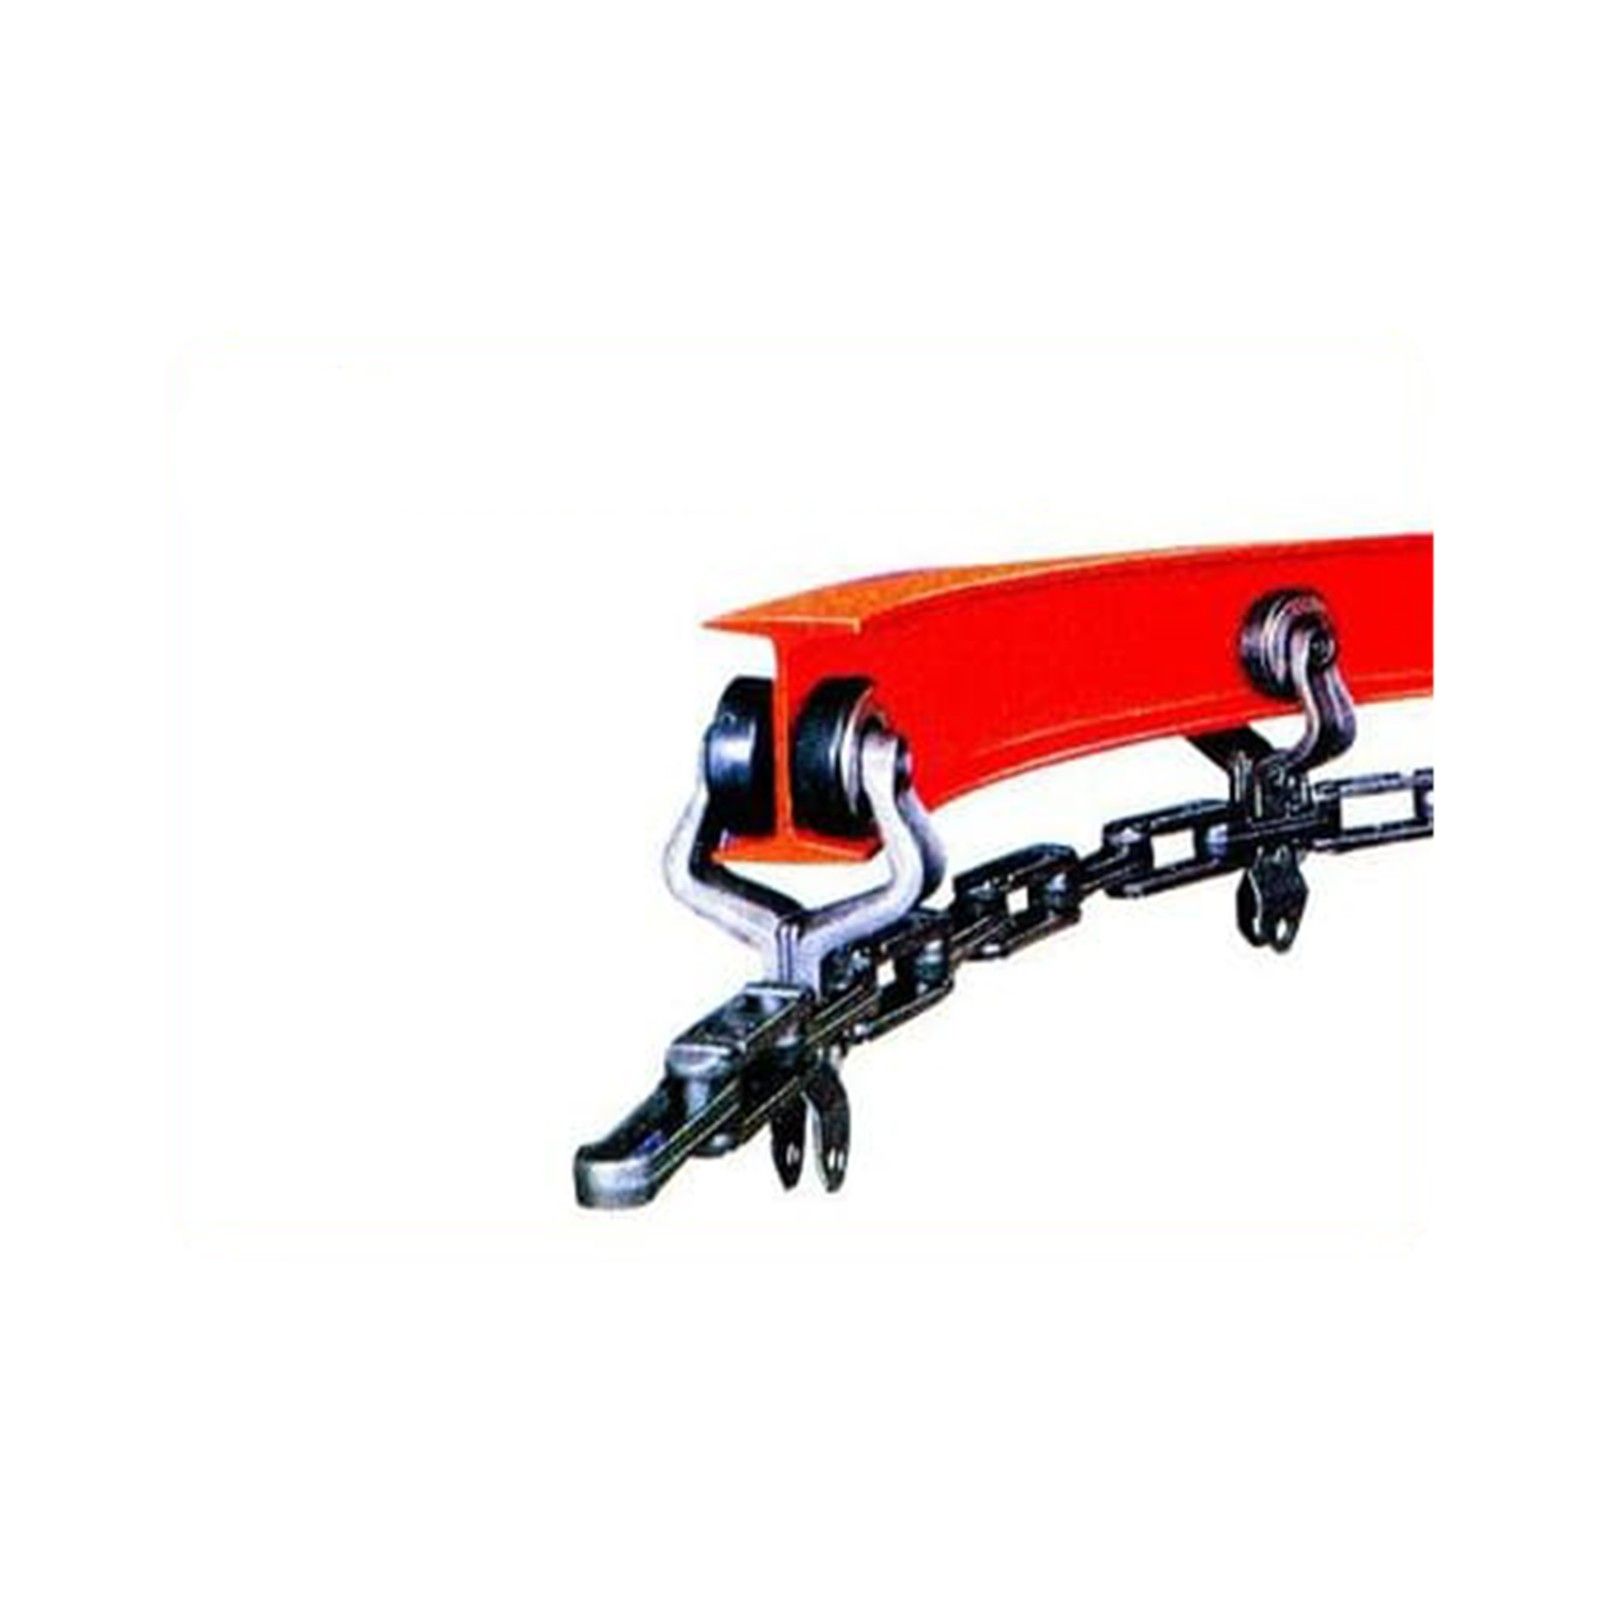
TROLLEY CONVEYOR
Trolley conveyors use overhead tracks and chain-driven trolleys to efficiently transport suspended loads.
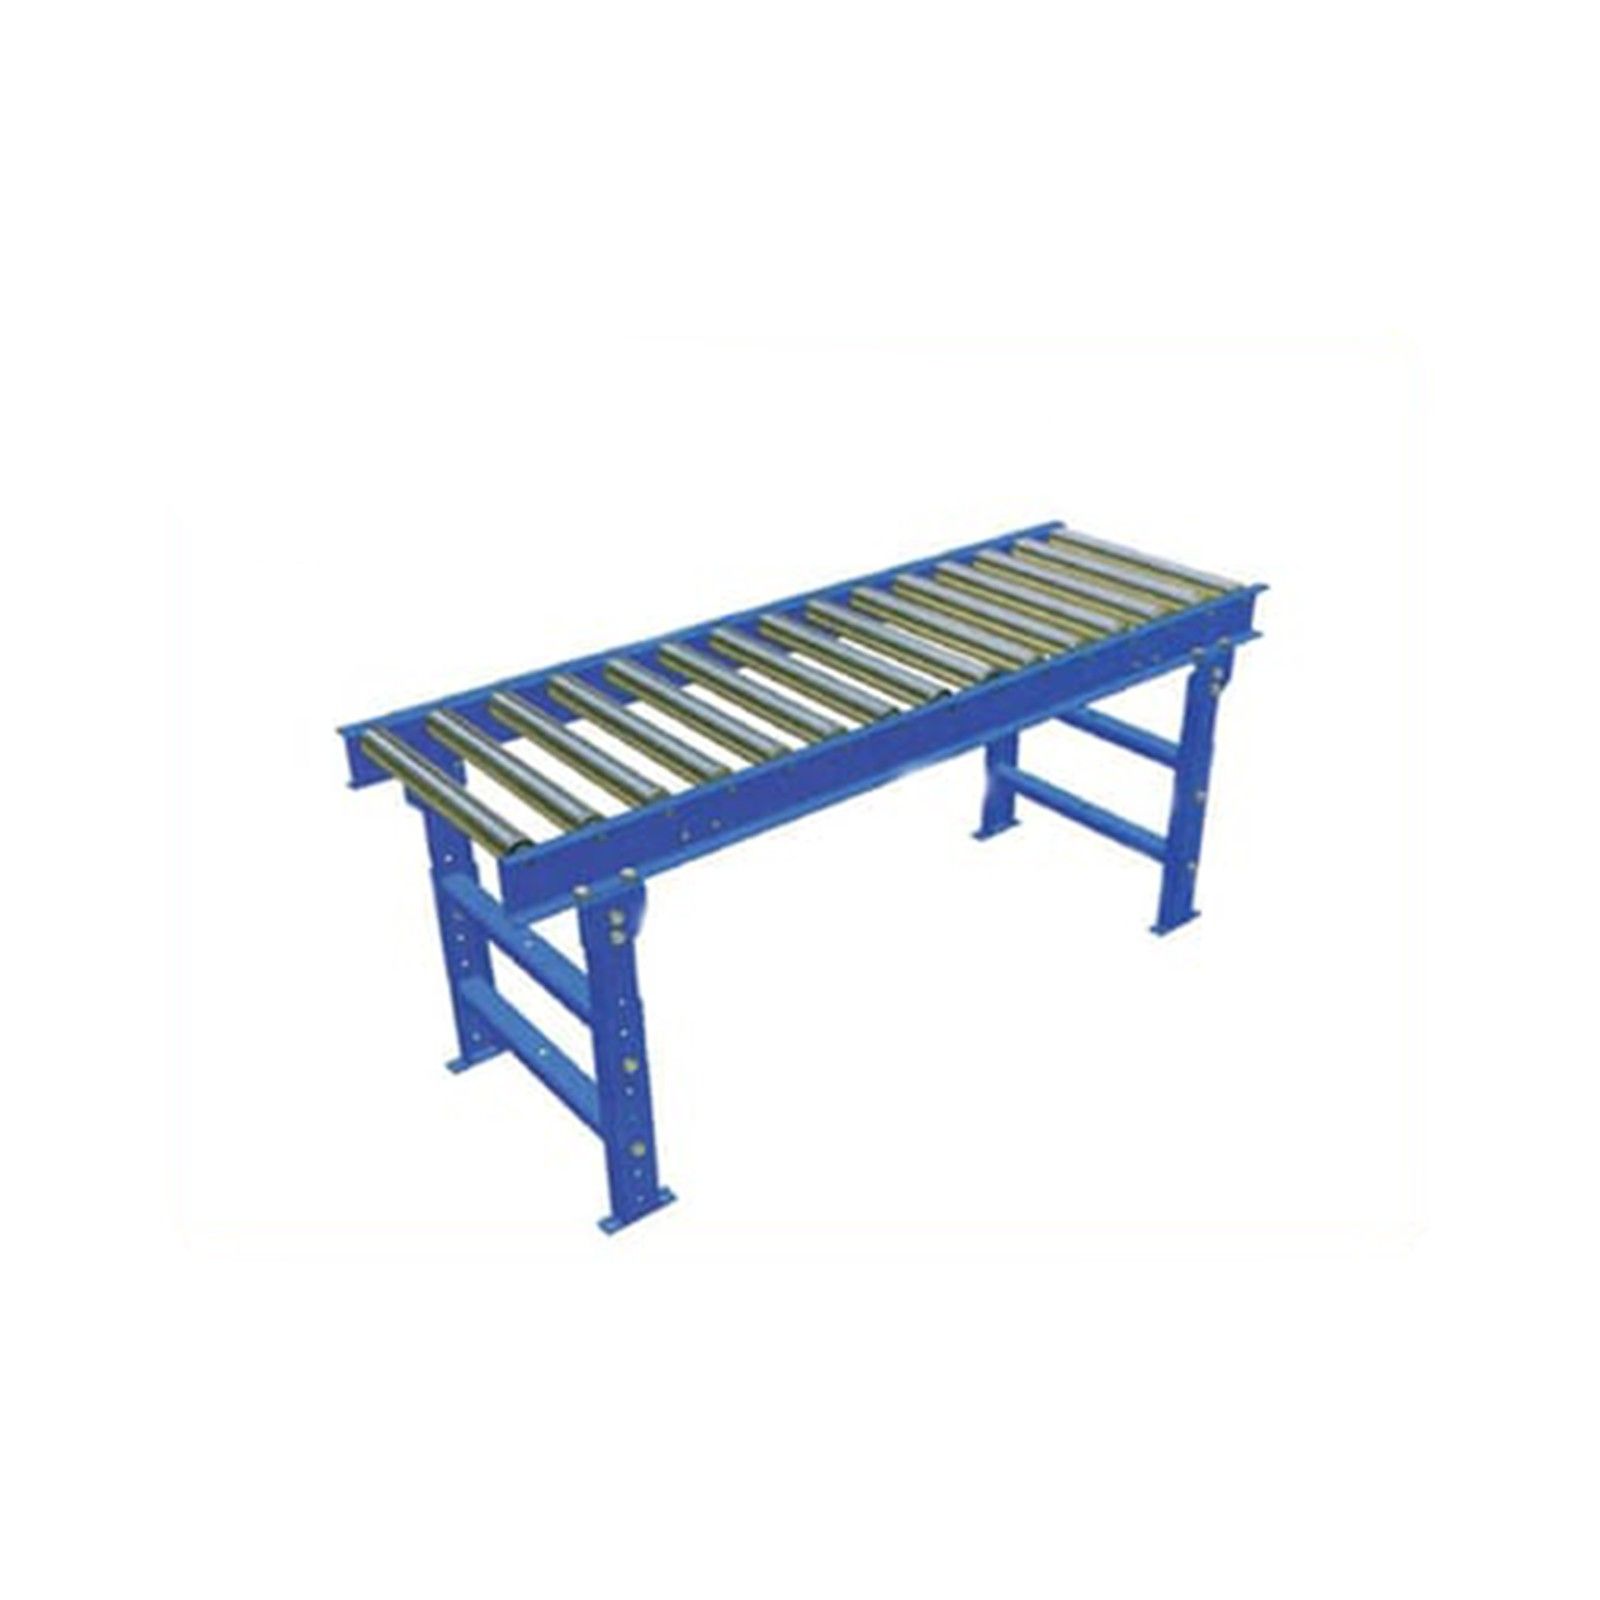
GRAVITY ROLLER CONVEYOR
Gravity roller conveyors provide simple, cost-effective material transport using gravity to move products along rotating rollers.
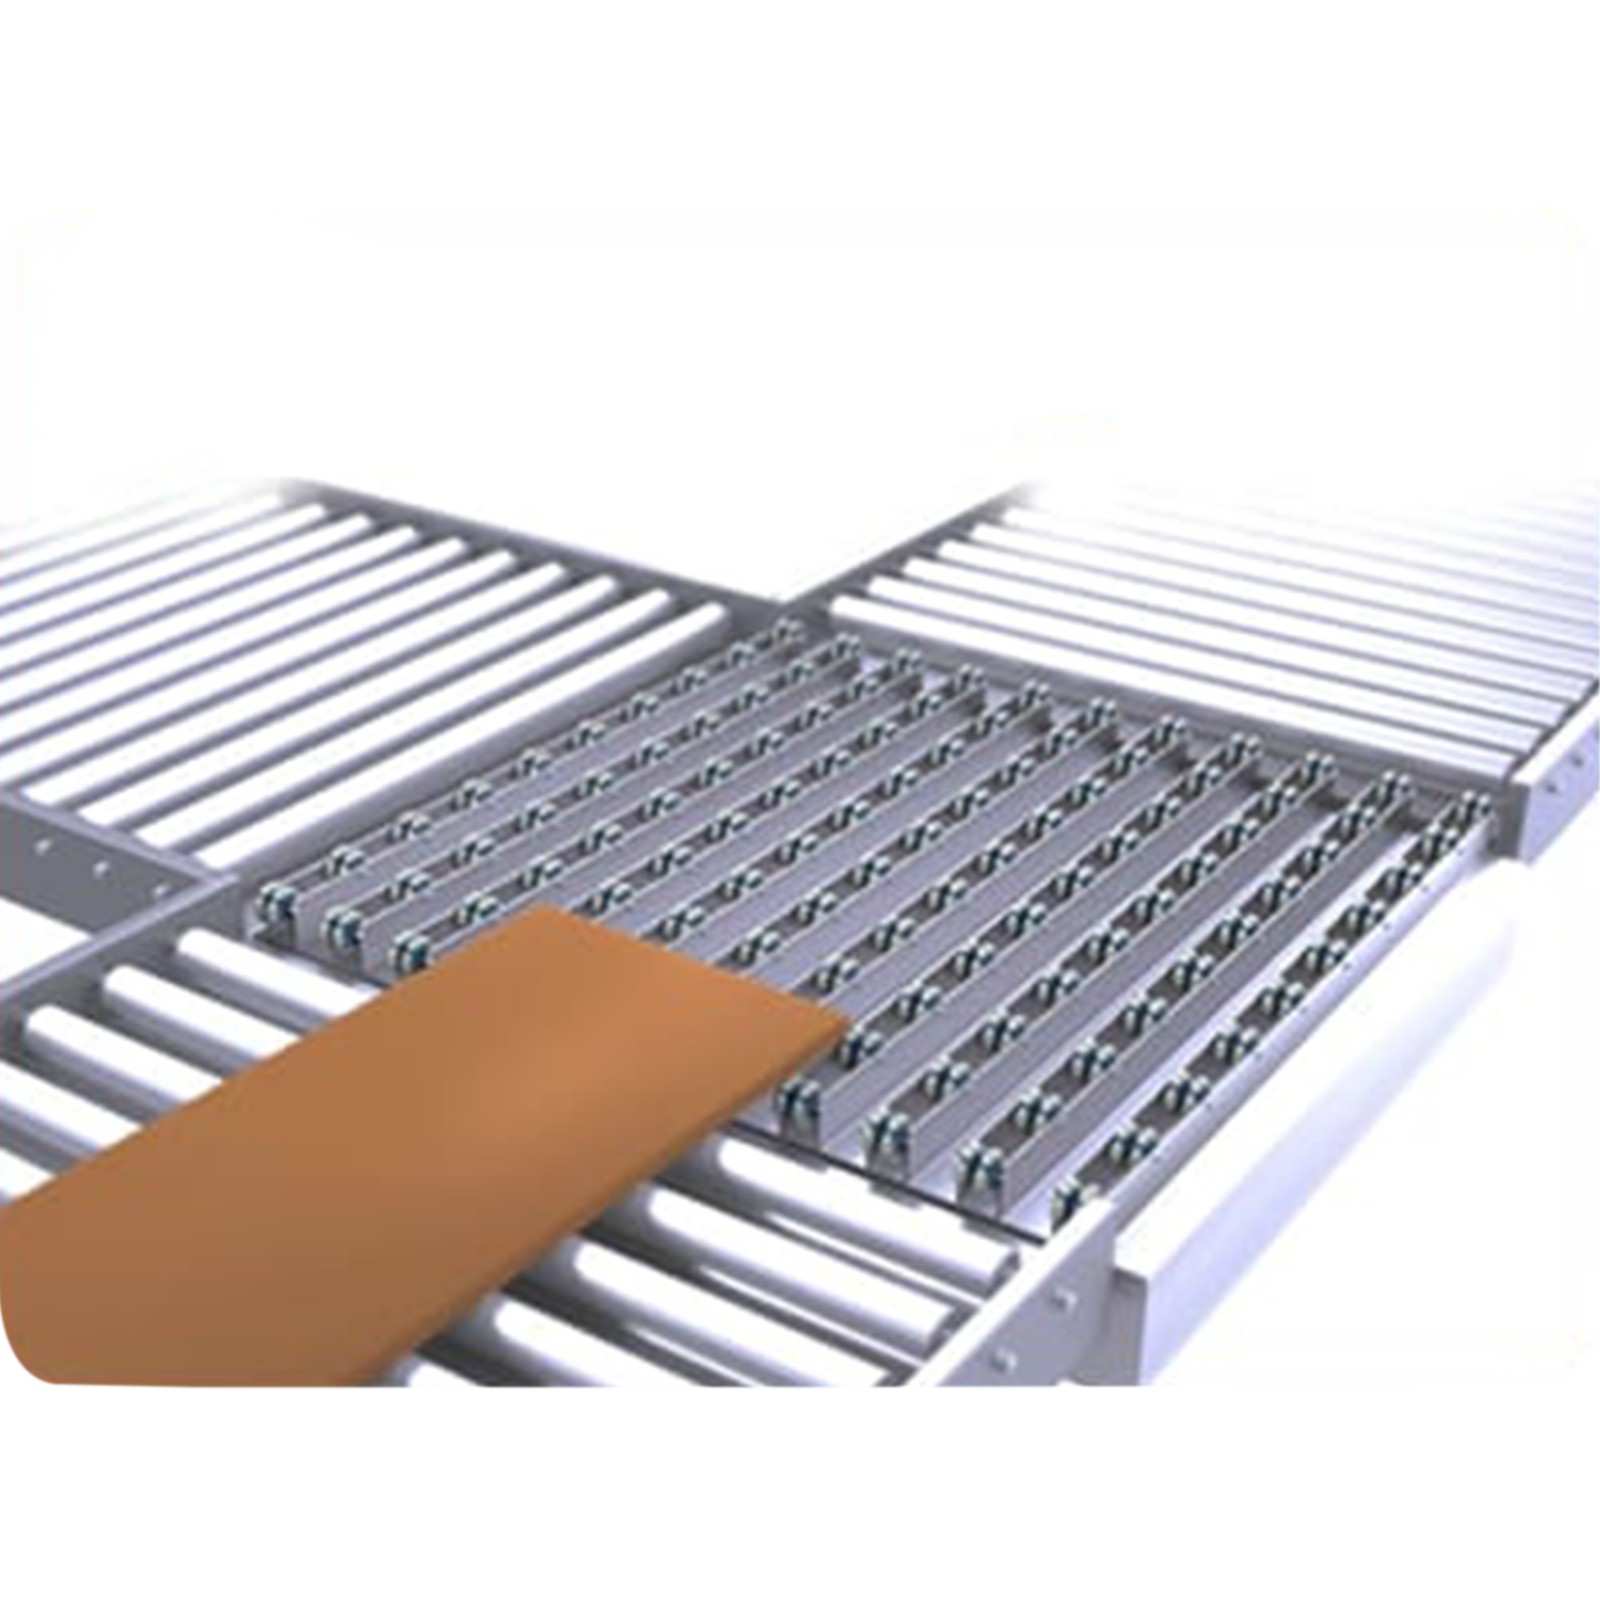
OMNI DIRECTIONAL CONVEYOR
Omnidirectional conveyors move products freely in multiple directions, enabling flexible and efficient material handling.
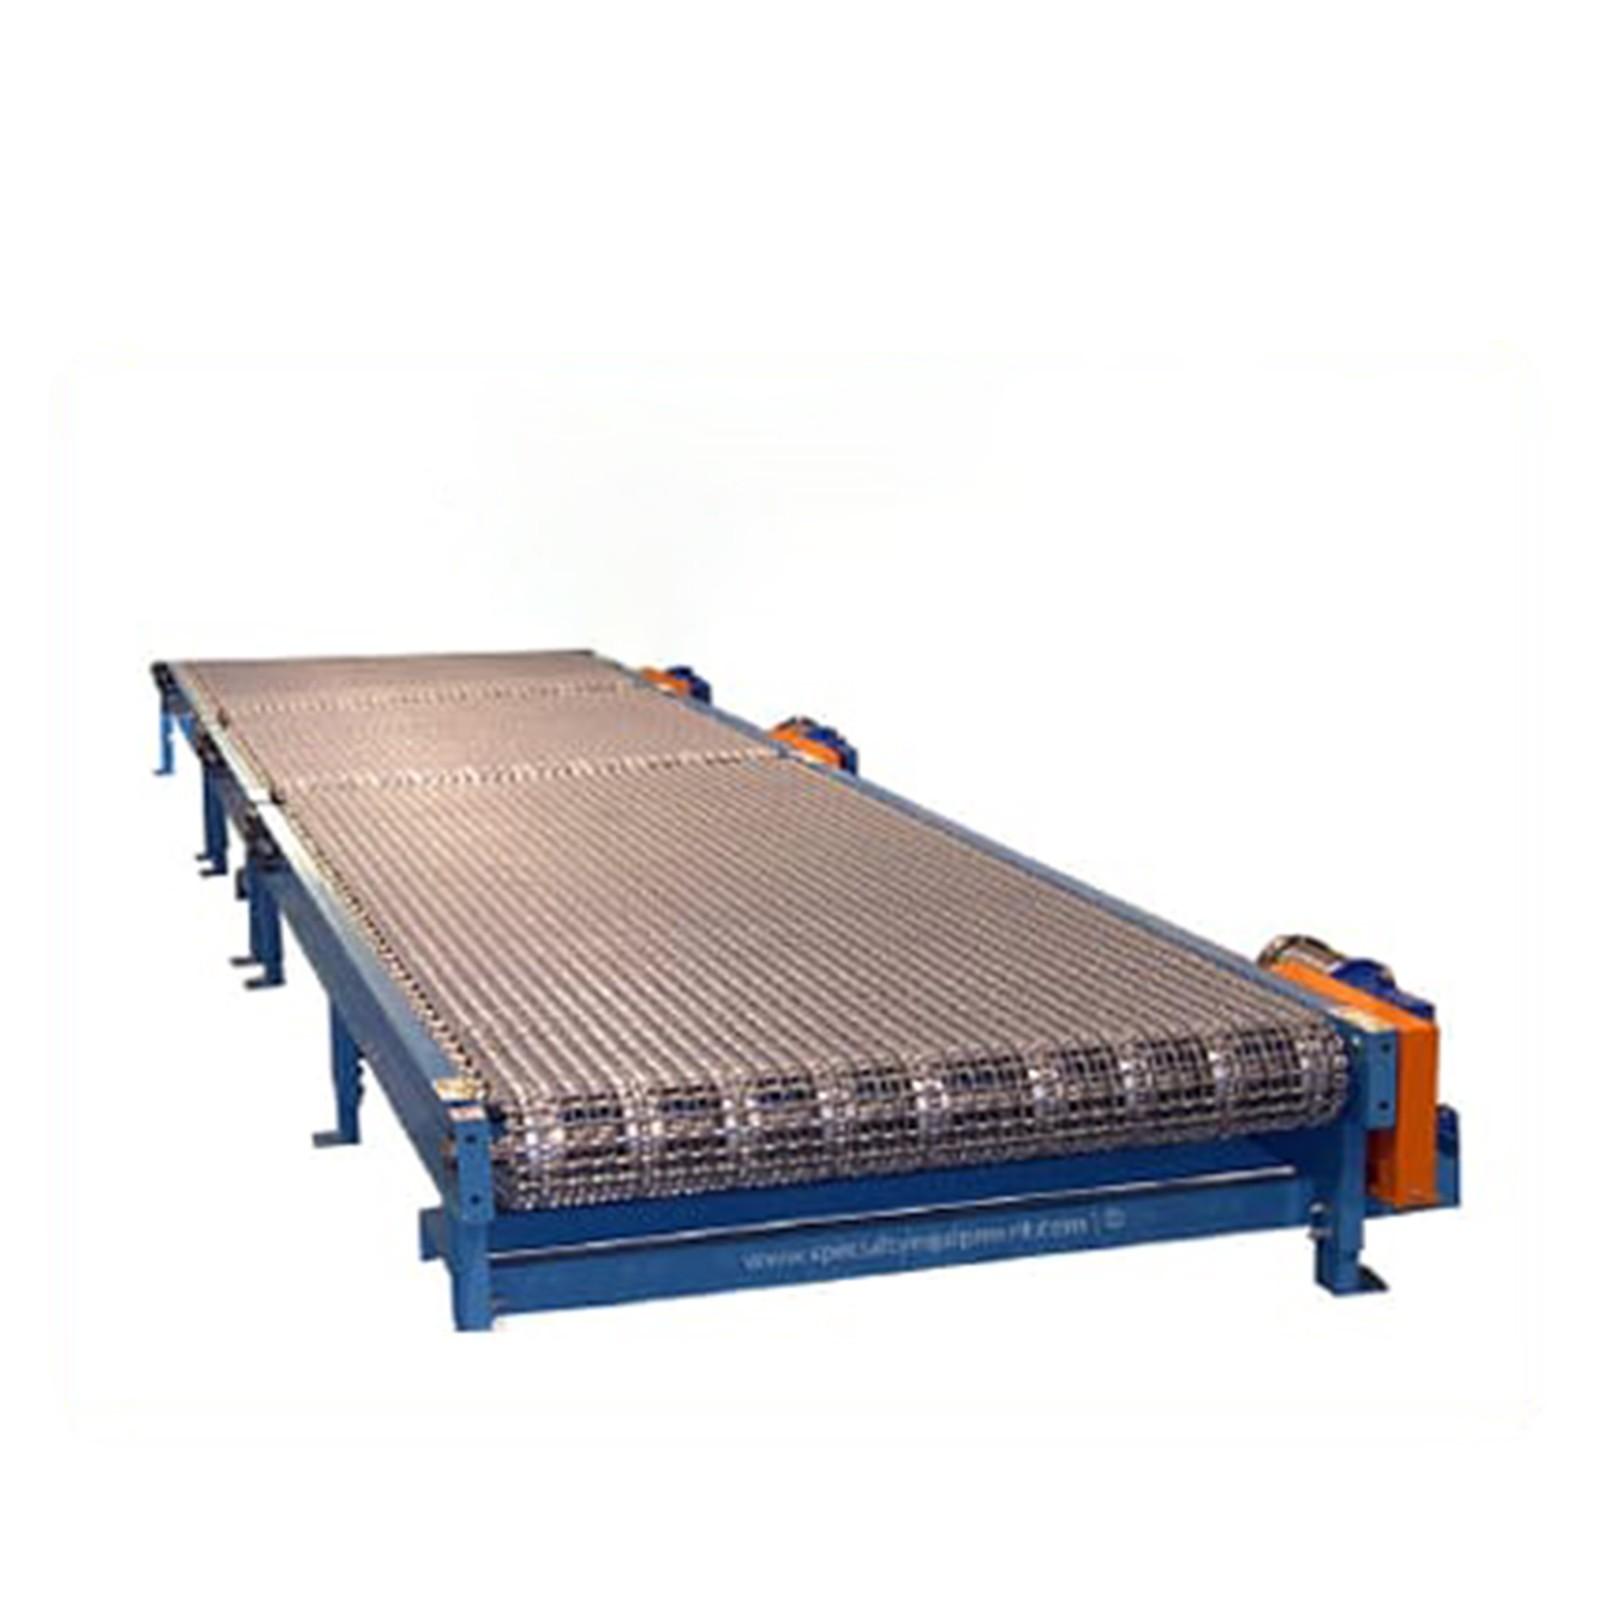
WIRE CONVEYOR BELT
Wire conveyor belts provide durable, flexible transport for production, heating, cooling, and freezing applications.

 +91 9606018355
 sales@safeautomations.com

 MODULAR BELT CONVEYOR
 WEDGE CONVEYOR